200 J
Toe Impact Certification
1100 N
Aramid Anti-Puncture Proof
1.2M+
Annual Footwear Pairs Exported
15-30 D
High-Volume Production Lead Time
Industrial Portfolio
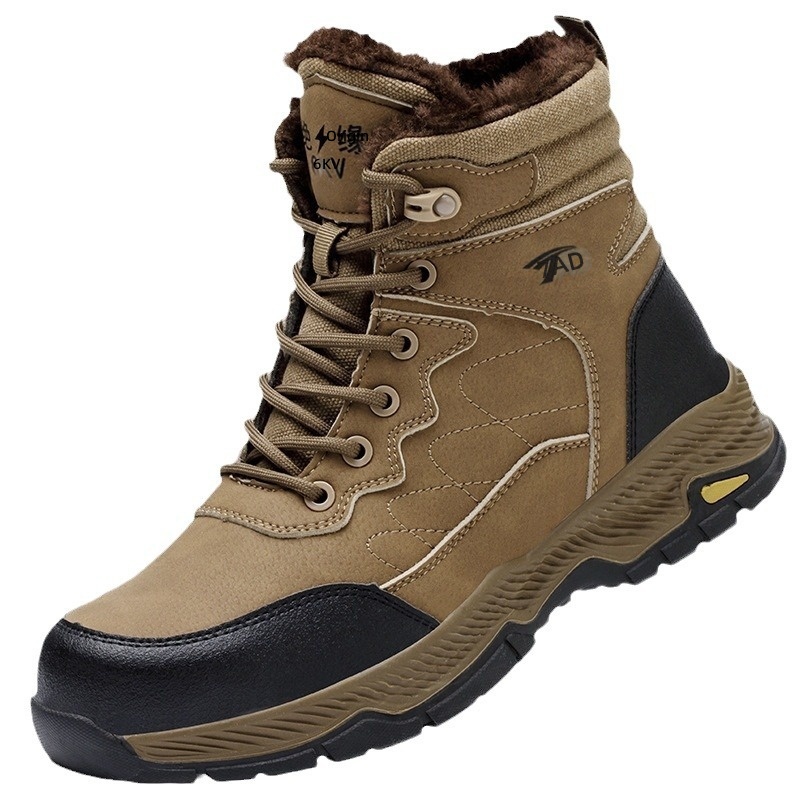
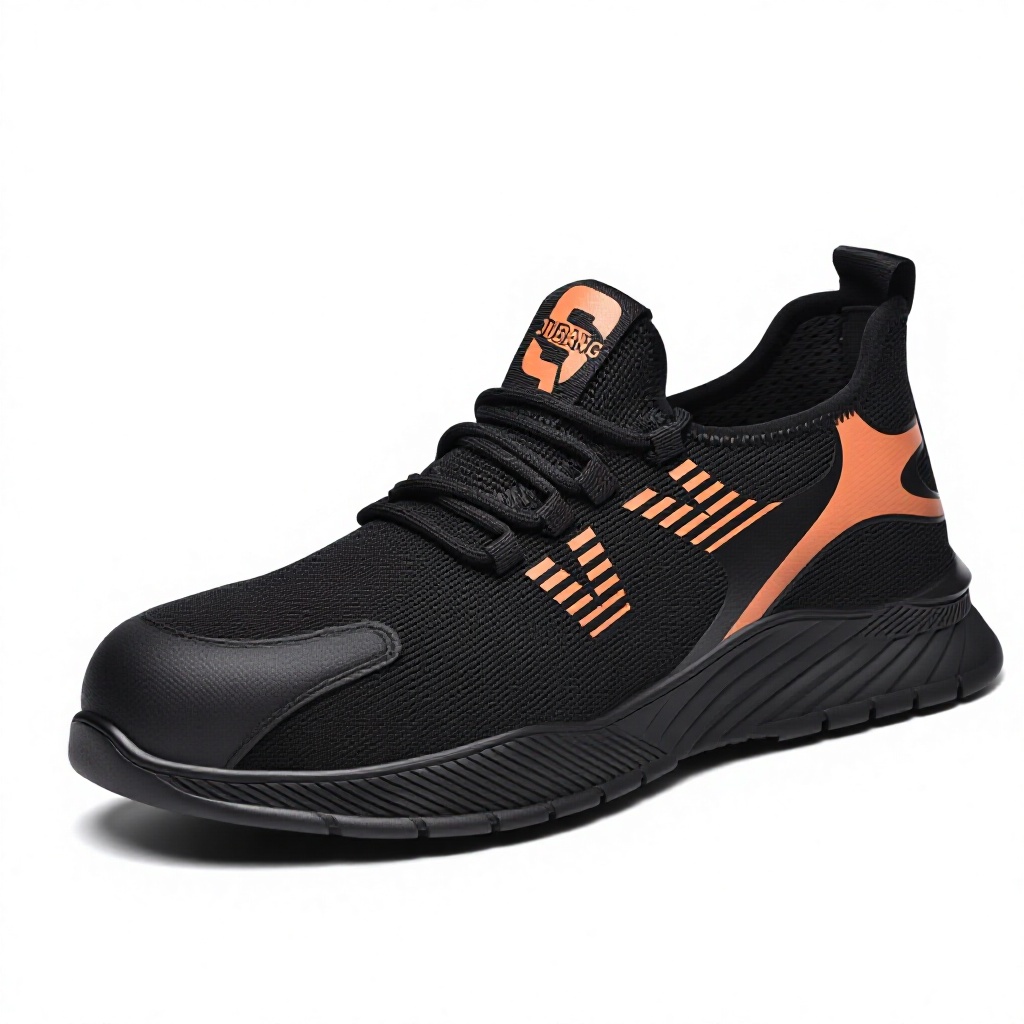
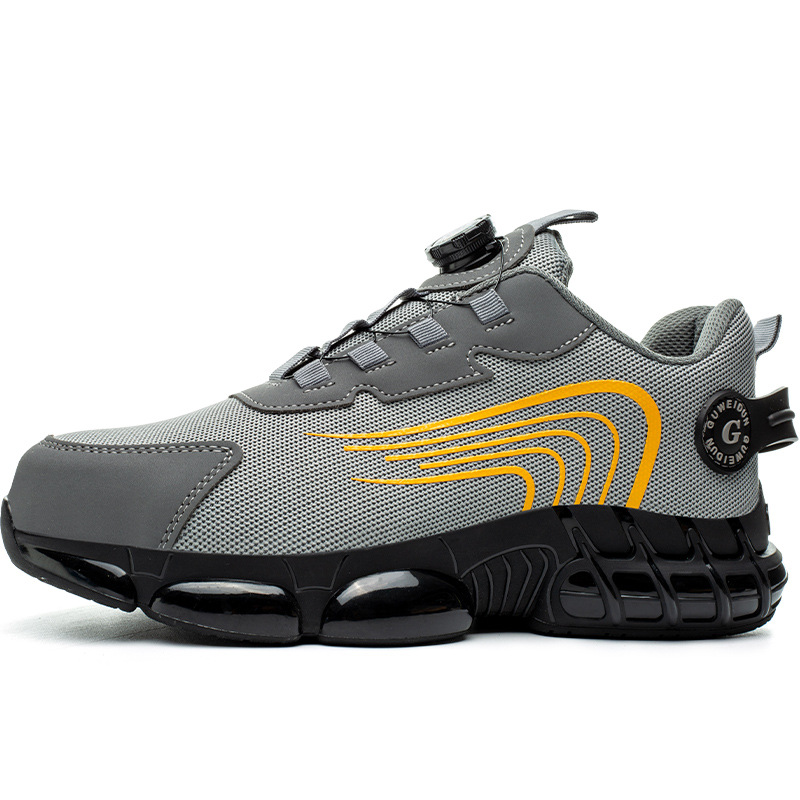
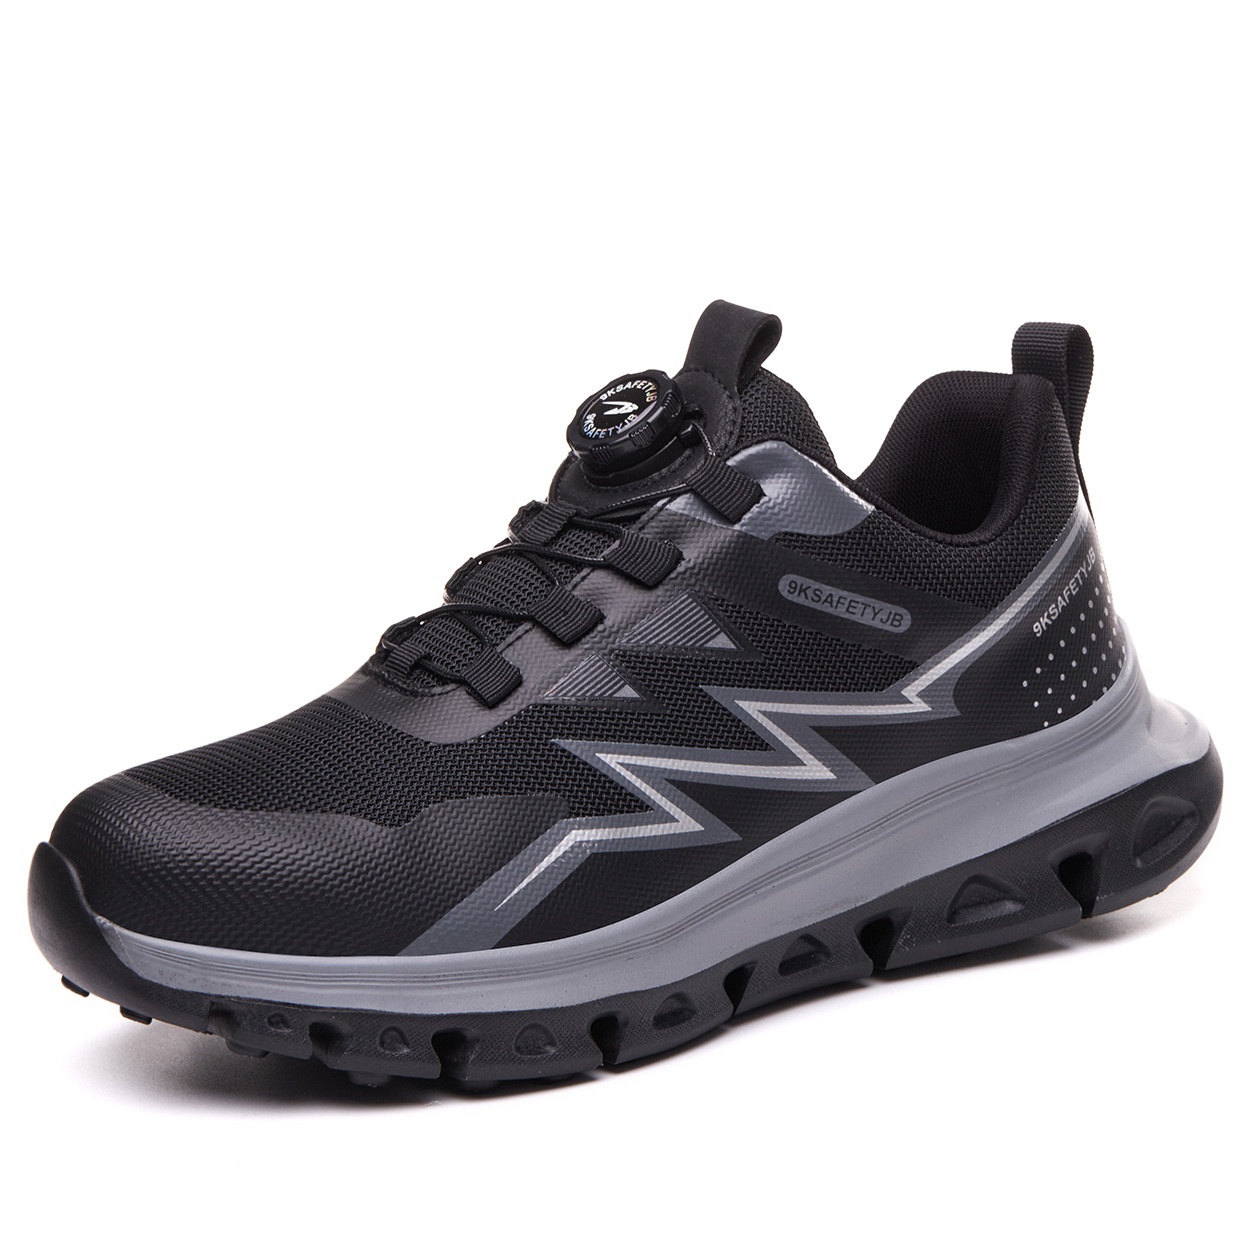
High-Performance Protective Footwear Catalog
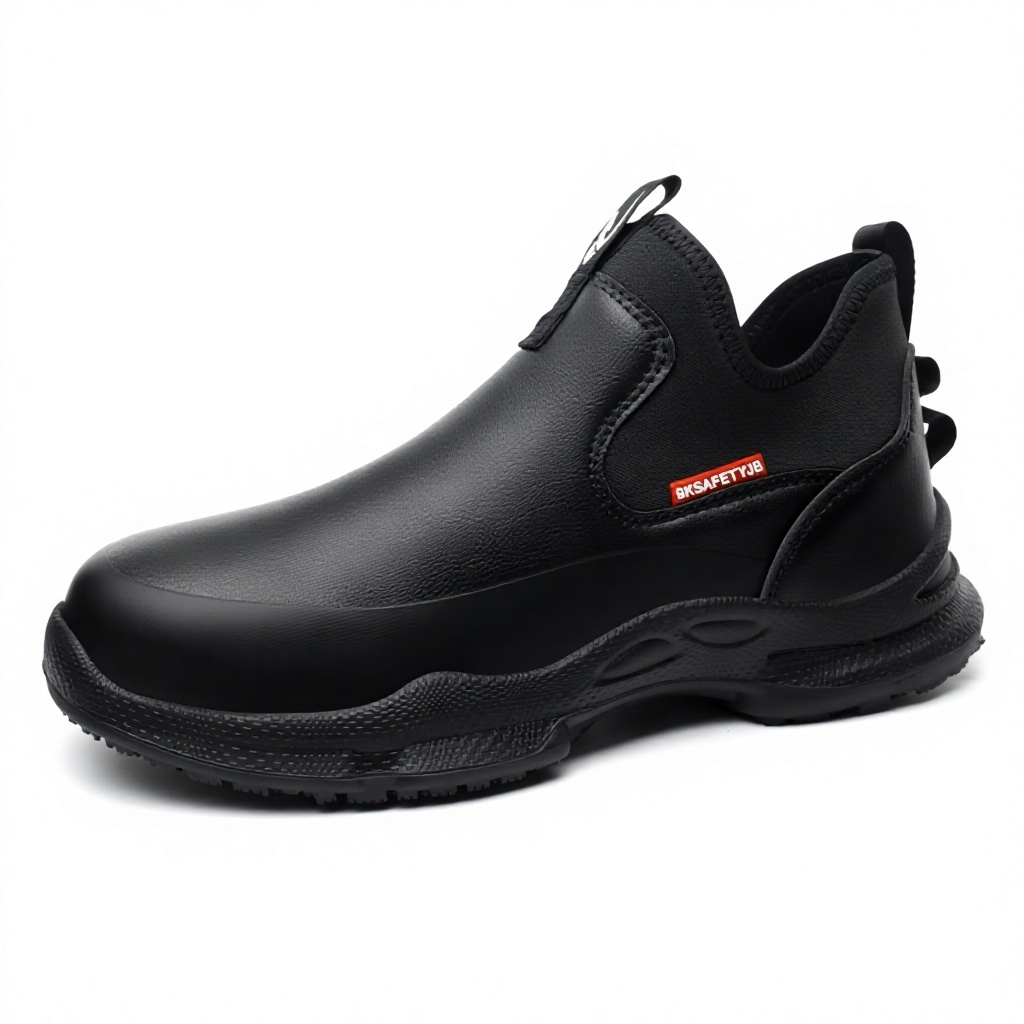
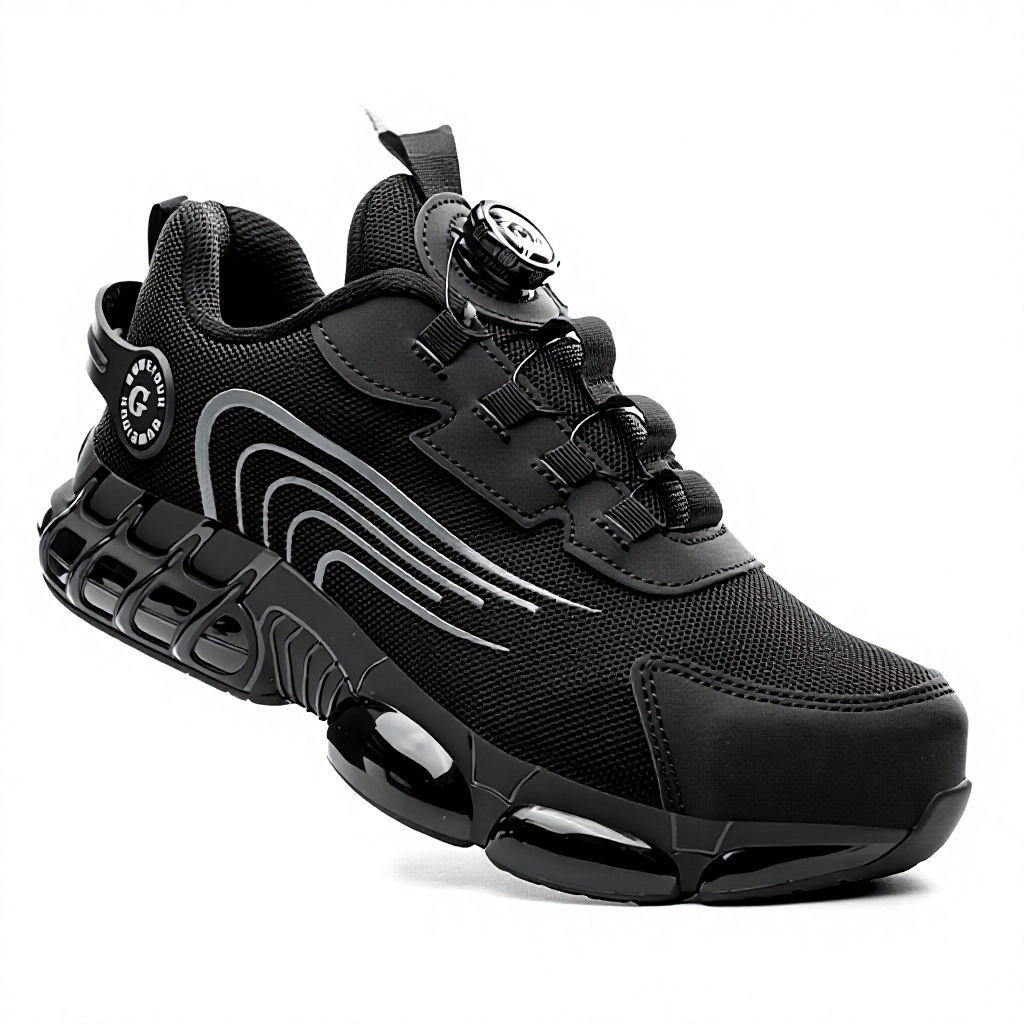
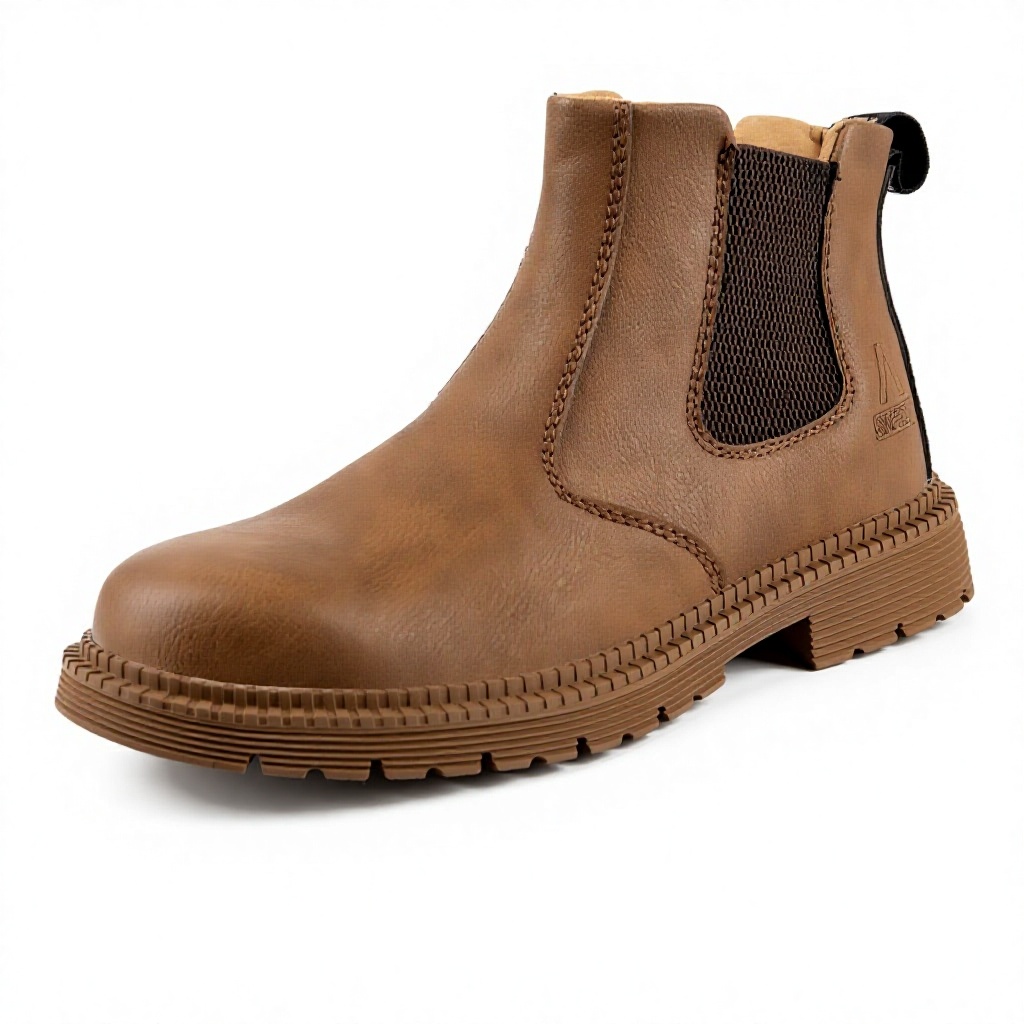
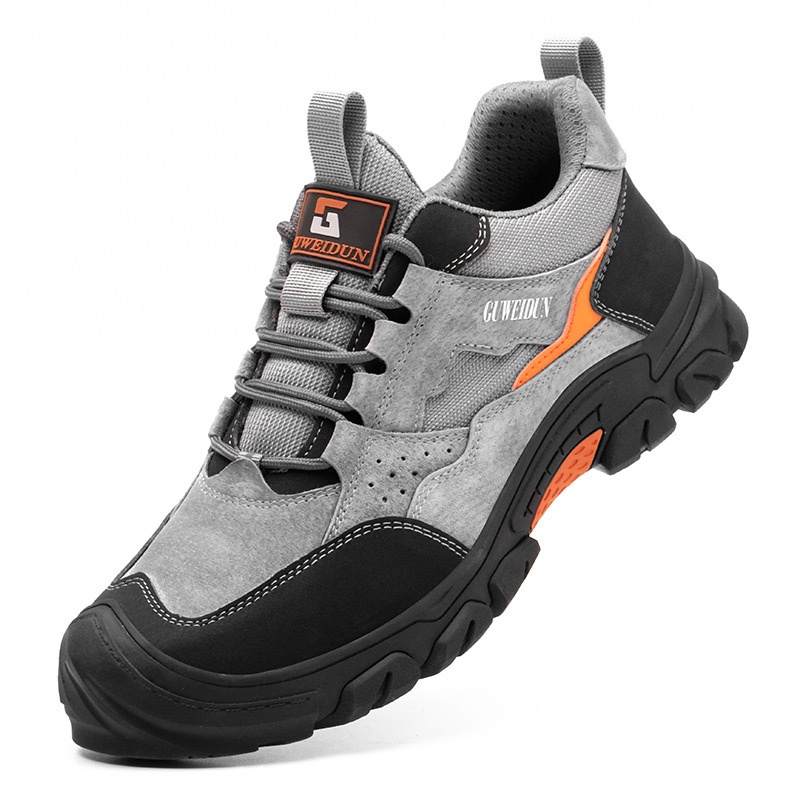
Engineered for hazardous terrain, chemical exposure, heavy fabrication yards, logistics, and industrial kitchens. Built to ASTM F2413-18 and EN ISO 20345 benchmarks.
Supply Chain Architecture
China Safety Footwear Manufacturing: Industrial Hubs & Technical Capabilities
A rigorous review of industrial clusters, manufacturing vulcanization vs injection processes, raw hide sourcing, and international certification architectures.
Regional Cluster Specialization
China's safety boot manufacturing is strategically segmented across regional clusters. Gaomi (Shandong) specializes in cost-optimized mass-volume injection footwear, commanding extensive raw leather supply chains. Wenzhou (Zhejiang) is the hub for precision PU/Rubber injection, high-spec polyurethane formulations, and EN ISO compliant laboratory tooling.
Meanwhile, Dongguan (Guangdong) leads in premium Goodyear-welted boots, military footwear, and sophisticated composite toe engineering targeting tier-one European and American brand distributors.
Sole Bonding: Injection vs Cementing
For B2B buyers, outsole adhesion integrity determines field failure rates. Direct Desma PU/PU Injection utilizes high-pressure liquid polyol and isocyanate reaction directly onto the lasted upper, eliminating adhesive lines and offering superior bond strength (>4.5 N/mm) resistant to hydrolysis.
In contrast, Cold Cementing using polychloroprene cements allows flexible pairing of lightweight EVA/Nitrile rubber compounds, ideal for agile low-top athletic safety footwear requiring high traction and slip resistance.
Tannery Traceability & REACH
Sourcing leather safety boots requires rigorous control over tanning chemistry. Top Chinese suppliers maintain direct partnerships with LWG (Leather Working Group) certified tanneries, ensuring chrome-free (wet white) or strictly calibrated chrome-tanned cowhide (1.8–2.2mm thickness) conforming to European REACH thresholds.
This completely eliminates banned substances including Chromium VI, pentachlorophenol (PCP), and harmful azo dyes, preventing costly customs confiscation at Rotterdam, Hamburg, or Long Beach ports.
| Material / Component | Technical Characteristics | Impact / Puncture Resistance | Weight per Boot (Est.) | Optimal Industry Application |
|---|---|---|---|---|
| Full-Grain Cowhide (1.8-2.0mm) | Dense natural grain fiber, extreme abrasion resistance, high breathability, natural water repellency with Scotchgard coating. | Tear strength >120 N; flex endurance >150,000 cycles without cracking. | 680g – 820g | Heavy construction, mining extraction, foundry, oil & petrochemical refineries. |
| Engineered Microfiber Leather | Polyamide non-woven matrix impregnated with polyurethane; hydrophobic, chemical and oil resistant, consistent grain thickness. | Exceptional tensile strength (>25 MPa), chemical wash resistant, zero surface peel. | 490g – 620g | Cleanrooms, automotive assembly lines, commercial food processing, hospitality kitchens. |
| Composite Polymer Toe Cap | Fiberglass or carbon composite matrix, 100% metal-free, non-magnetic, zero thermal and electrical conductivity. | 200 Joule drop-mass impact, 15 kN static compression (ASTM F2413 / EN 12568). | 35g – 45g (Cap only) | Airports, electrical utility maintenance (EH rated), cold storage logistics facilities. |
| Forged Steel Safety Toe | Heat-treated high-carbon steel, ultra-thin cross section maximizing internal toe box room, epoxy coated anti-corrosion. | Exceeds 200 Joules impact, superior puncture point load resistance against sharp edge drops. | 85g – 95g (Cap only) | Structural steel erection, heavy machine manufacturing, scrap yards, rail infrastructure. |
| Woven Aramid / Kevlar Midsole | Multi-layered ballistic aramid woven composite, stitch-bonded directly under the insole; zero dead zones across outsole perimeter. | Resists >1100 N perpendicular spike penetration (zero tip penetration under EN 22568-4). | 50g (Midsole) | Roofing, municipal recycling yards, warehousing, urban demolition sites. |
Regulatory Procurement Note: EN ISO 20345:2022 vs. ASTM F2413-18
The revised European standard EN ISO 20345:2022 introduces refined puncture categories: P (metallic 4.5mm nail), PL (non-metallic 4.5mm nail), and PS (non-metallic 3.0mm small-diameter nail), alongside slip resistance designation SR. Chinese OEM manufacturers have updated tooling and injection mold texturing to ensure all export batches pass both SATRA and CTC laboratory inspections with documented type-examination certificates.
Market Intelligence
Future Procurement Trends in Industrial Footwear (2025–2030)
Anticipate supply chain shocks, regulatory carbon reporting, material lightweighting, and automated production shifts shaping enterprise procurement.
Microfiber Replacement of Split Leather
Rising tanning effluent costs and corporate ESG pressure are driving a 28% annual shift from animal split/action leather to advanced waterborne polyurethane microfiber. Microfiber eliminates biological defect waste, delivers 98% roll yield, and withstands harsh commercial chemical detergents.
Scope 3 Carbon Accounting
Global enterprises are mandating Product Carbon Footprint (PCF) disclosures under ISO 14067. Tier-1 Chinese manufacturers are adopting bio-based thermoplastic polyurethanes (TPU) derived from castor oil, recycled PET laces, and circular rubber compounds with up to 35% reclaimed crumb.
Ergonomic Ultra-Lightweighting
Occupational health data confirms that daily worker fatigue is directly correlated with boot weight. Next-generation safety shoes integrate supercritical nitrogen-foamed EVA and expanded TPU (E-TPU) midsoles, shaving average boot weight from 750g to under 430g while returning 65% energy rebound.
Near-Zero Defect Automated Desma Lines
Labor demographic shifts in coastal China have accelerated the installation of multi-station robotic injection carousels and computerized roughing machines. Automated lasting guarantees consistent seam margins, eliminating human error in cement activation and welt stitching.
Factory Competency
Why International Importers Partner with Our Manufacturing Network
Combining vertically integrated component fabrication, in-house accredited laboratories, and transparent production governance.
In-House Mechanical Testing Lab
Every single batch undergoes rigorous pre-shipment destructive testing: 200J drop-mass impactors, 15kN hydraulic crushers, 100,000 cycle flexing machines, and electrical resistance static testing meters calibrated directly to UKAS standards.
Flexible OEM / ODM Customization
From custom embossed logos, branded metal hardware, and localized warning labels to tailored lasts for European (wider ball girth) vs. Asian anthropometric foot shapes. Fast-track prototyping delivers sample pairs in 5 to 7 working days.
Strict Supply Chain Traceability
Every roll of raw cowhide, spool of aramid thread, and batch of polyurethane elastomer carries unique material lot numbers traceable back to raw ingredient blending certificates, preventing sub-tier supplier degradation.
High-Volume Capacity & Scalability
Operating 6 automated injection lines and 4 cold-cement assembly tracks yielding over 120,000 pairs monthly. Scalable production buffers enable container-load order fulfillments within 25–35 days even during peak pre-winter surges.
Complete Export Documentation
We provide full customs compliance dossiers: Form A, Certificate of Origin, REACH SVHC declarations, third-party CE Certificates (Module B + C2/D), and customized barcoded carton labels for seamless 3PL distribution.
Comprehensive Incoterms & Payment
Supporting FOB Ningbo/Qingdao/Shenzhen, CIF destination ports, DDP warehouse delivery, backed by flexible B2B financing terms including L/C at sight, T/T staged milestones, and escrow trade assurance options.
Procurement Inquiries
Frequently Asked Questions: Safety Footwear Sourcing & Compliance
Clear, direct answers to common questions regarding minimum order quantities, testing protocols, custom lasts, and international import logistics.
? What is the standard Minimum Order Quantity (MOQ) for custom safety footwear?
Standard OEM production with customized leather colorways, embossed branding, and branded insoles typically requires 500 to 1,000 pairs per style across 5 to 7 shoe sizes. For completely custom outsole injection molds requiring new CNC aluminum tooling, initial prototype molds range between 800 and 1,500 pairs per run to amortize tooling investments efficiently.
? How do you guarantee that mass production matches the certified test sample?
We operate under ISO 9001 quality systems and utilize an AQL 1.5/2.5 inspection threshold. Certified master swatches and component specification sheets are locked in production Golden Samples. Additionally, factory technicians perform daily in-process batch tests for toe drop resistance, interlayer bond adhesion, and leather flexing before packaging clearance.
? Steel Toe vs. Composite Toe: Which should we specify for our tender?
Specify Steel Toes if your priority is minimal cross-sectional thickness (sleeker boot aesthetic), lowest unit manufacturing cost, and maximum protection against ultra-sharp structural steel edge impacts. Specify Composite (Fiberglass/Carbon) Toes for workers in sub-zero freezer logistics (no thermal bridging), electricians (dielectric non-conductive), or sites with security metal detectors.
? What is the shelf life of PU injection soles in humid warehouse climates?
Polyurethane is subject to atmospheric hydrolysis if formulated with polyester polyols in warm, high-humidity storage environments. For export to tropical regions (Southeast Asia, Gulf Region, Latin America), our chemists utilize polyether-based polyols and anti-hydrolysis stabilizer additives, extending storage shelf-life beyond 36 to 48 months without degradation.
? Can you manufacture safety footwear under our domestic market standards (e.g., AS/NZS or CSA)?
Yes. Our engineering department routinely works with Australian/New Zealand (AS/NZS 2210.3), Canadian (CSA Z195 with Grade 1 green triangle and white rectangle ohm patch), and American (ASTM F2413 EH dielectric 18kV) testing matrices. All required component inserts (such as omega-rated midsoles and specialized lasts) are sourced and certified accordingly.
? What is the typical sampling, laboratory certification, and delivery timeline?
Physical functional samples are dispatched via DHL/FedEx within 5 to 10 days. If full European notified body certification (CE type-examination via agencies like Intertek, SGS, or CTC) is required for a new mold, laboratory testing takes approximately 4 to 6 weeks. Standard mass container production requires 25 to 35 calendar days from deposit approval.
Connect with Senior Industrial Footwear Engineers
Whether you require tender-ready EN ISO 20345:2022 compliant prototypes, private label branding, or full container supply chain pricing, our technical team provides rapid quotations within 24 hours.