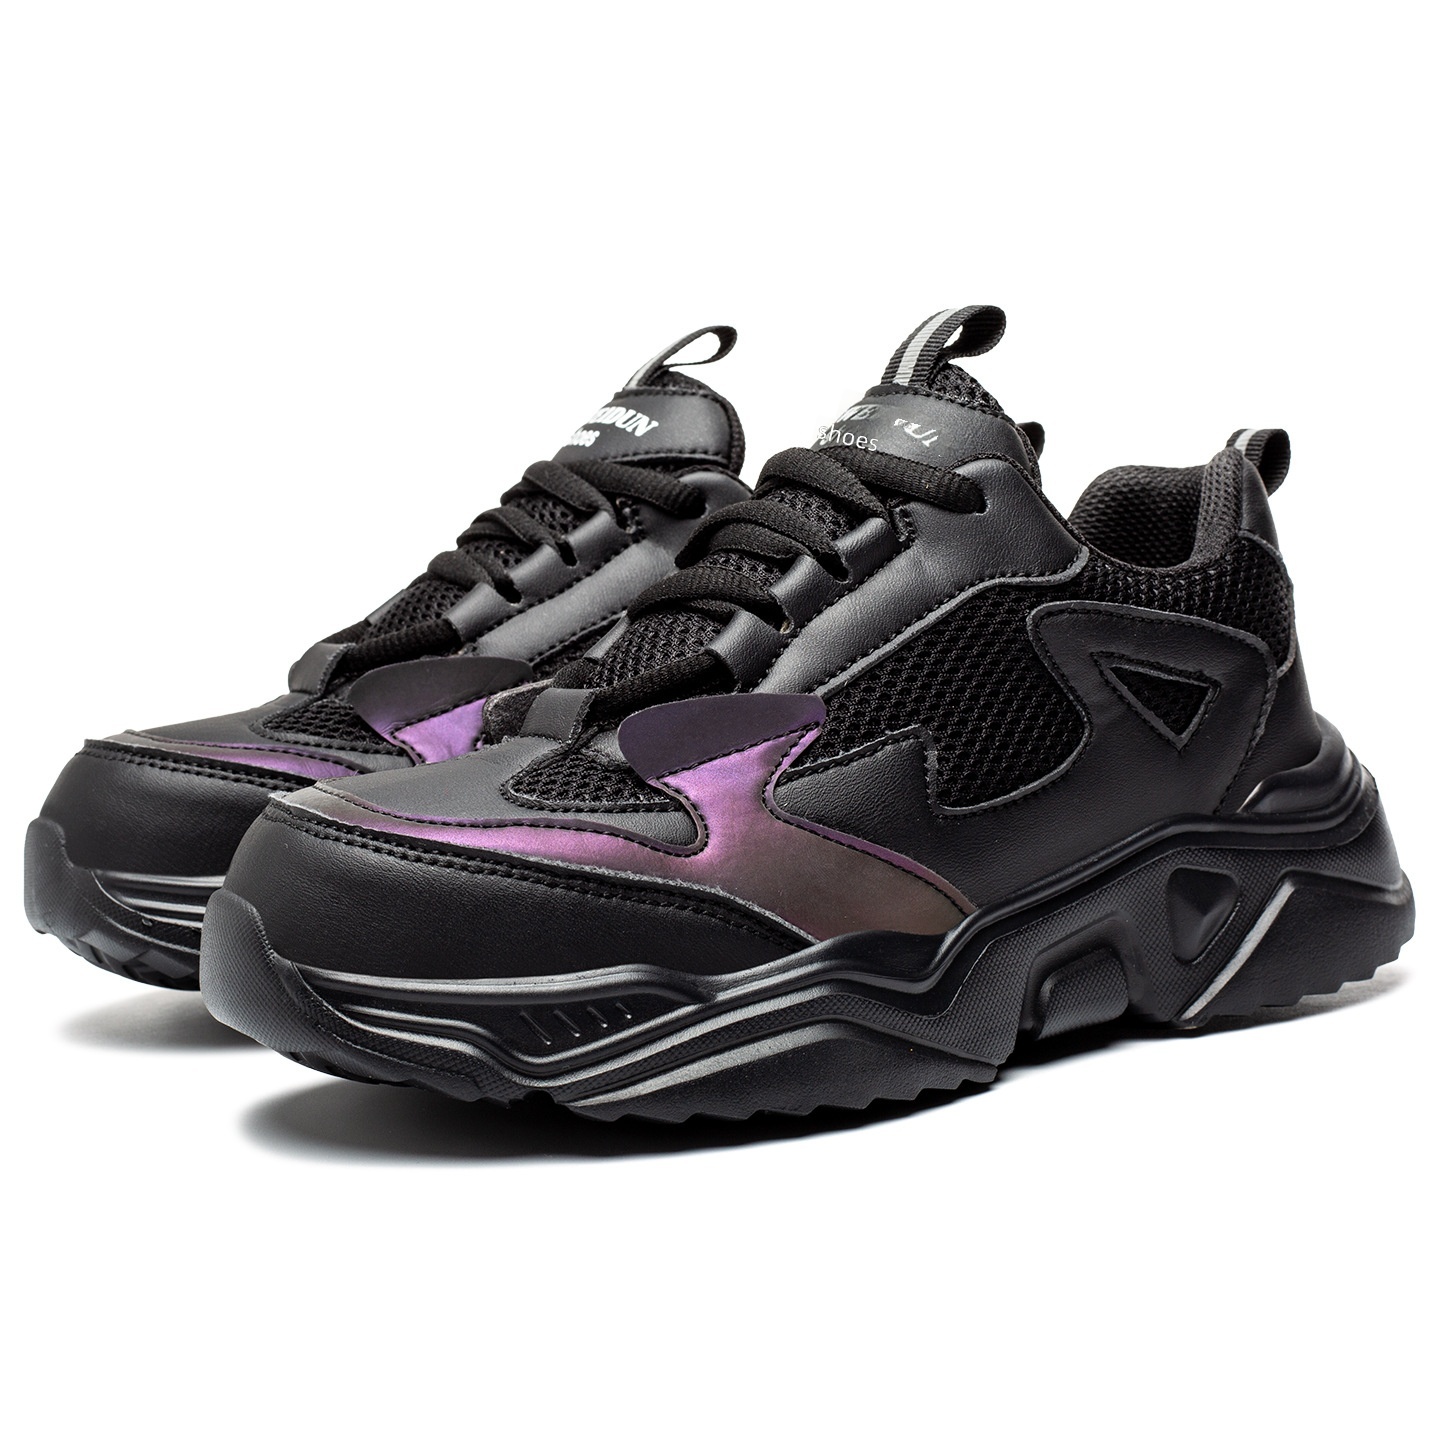
Engineered Safety Footwear Showcase
Integrated anti-penetration, impact shielding, and petrochemical corrosion-resistant solutions designed for the heavy industrial, architectural, and mechanical manufacturing sectors.
Men's Summer Safety Shoes Steel Toe Fly-knit Mesh Breathable Anti-smash Anti-puncture All Seasons
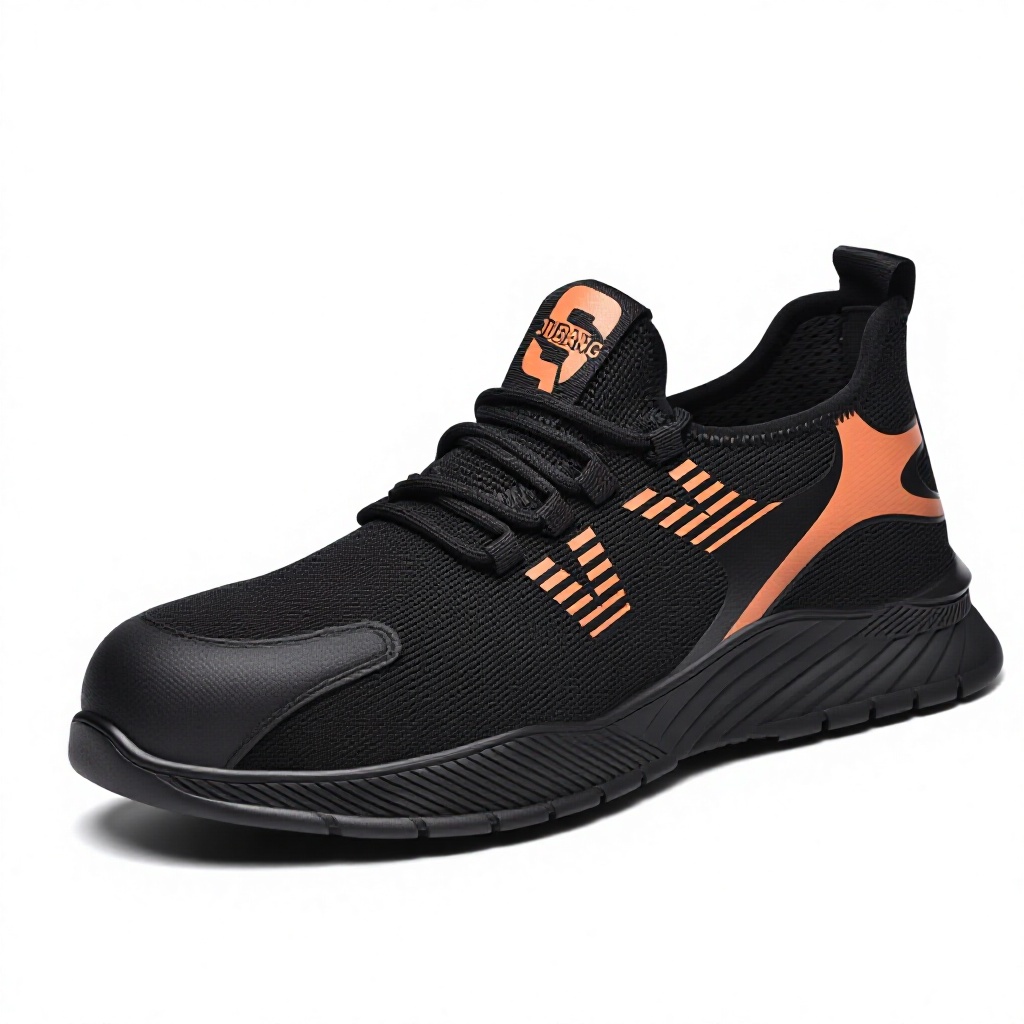
Men's Steel Toe for Fabric Low Top Summer Breathable & Comfortable Labor Protection Shoes for Architectural Industry
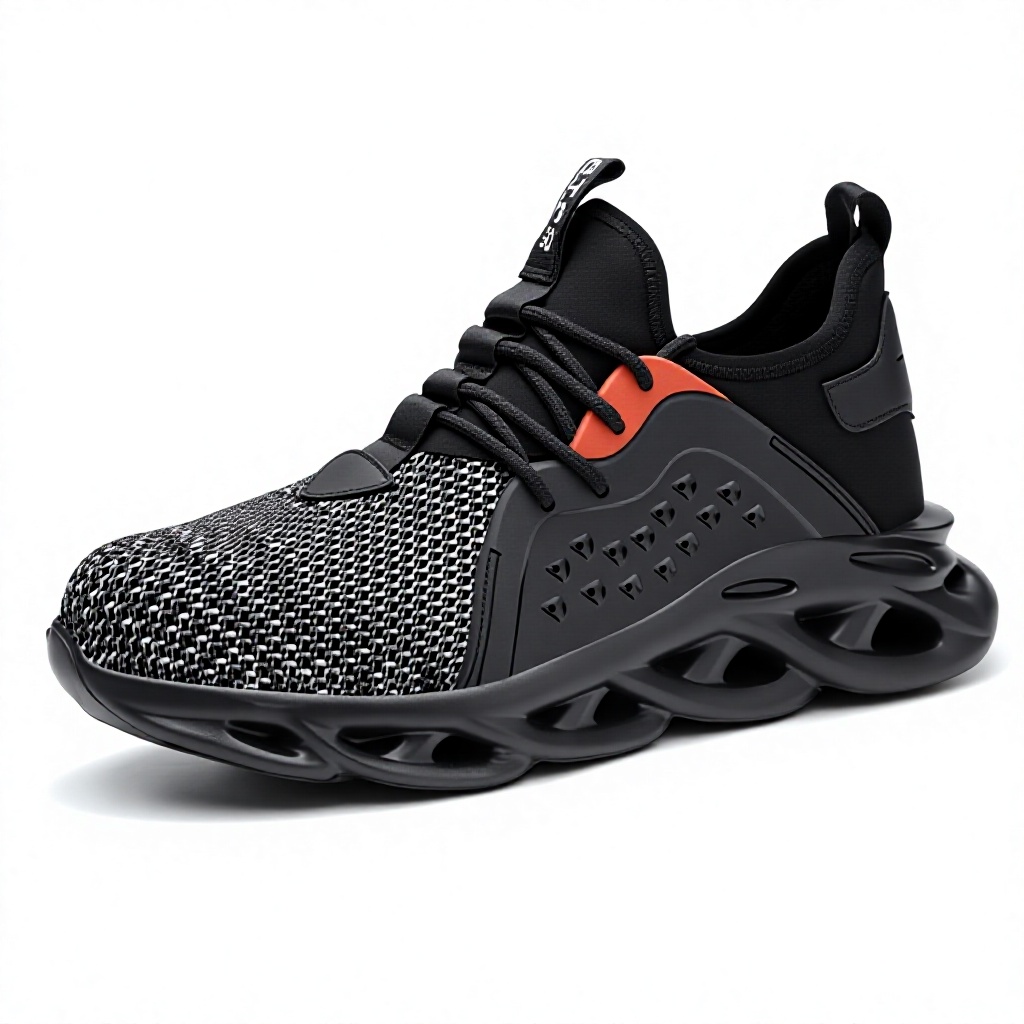
Men's Summer Work Safety Shoes Low Top Breathable Odor-Resistant Steel Cap Anti-Smash Anti-Puncture Ultra-Lightweight
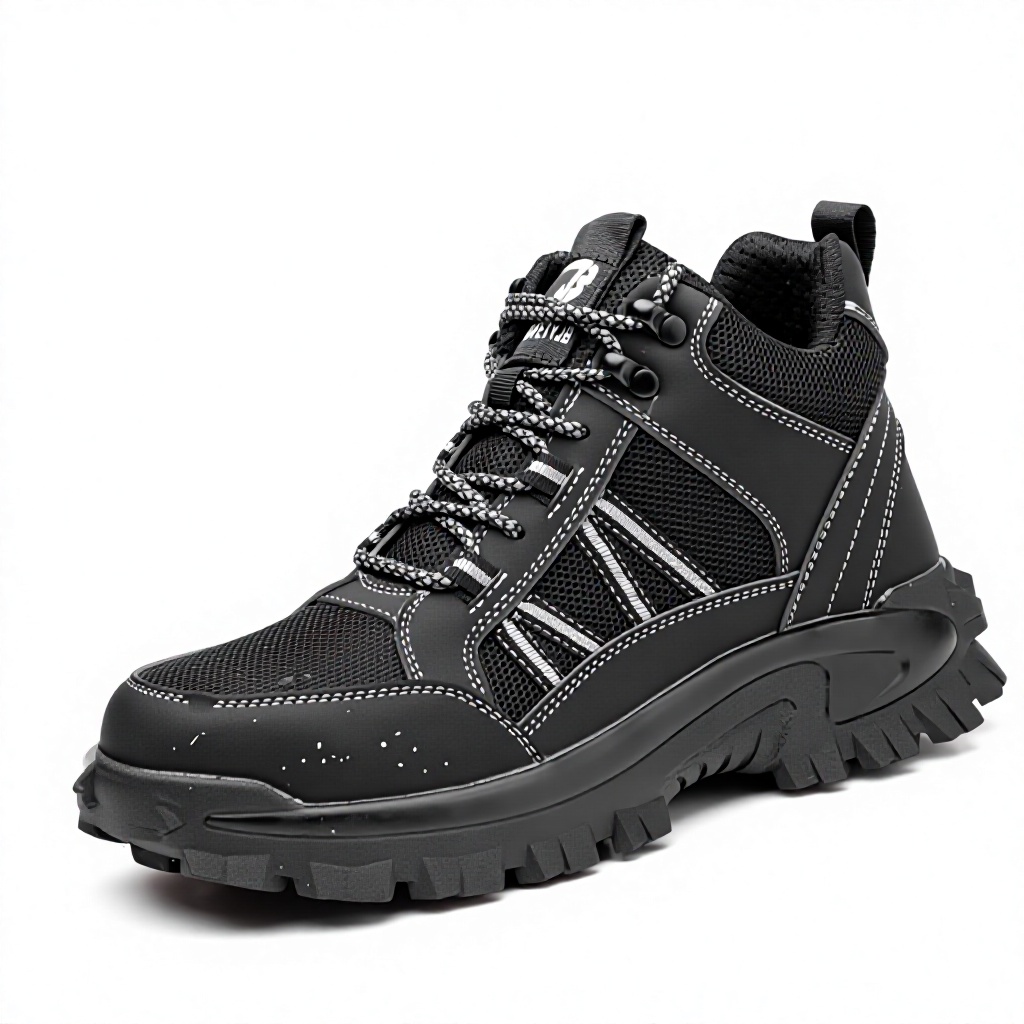
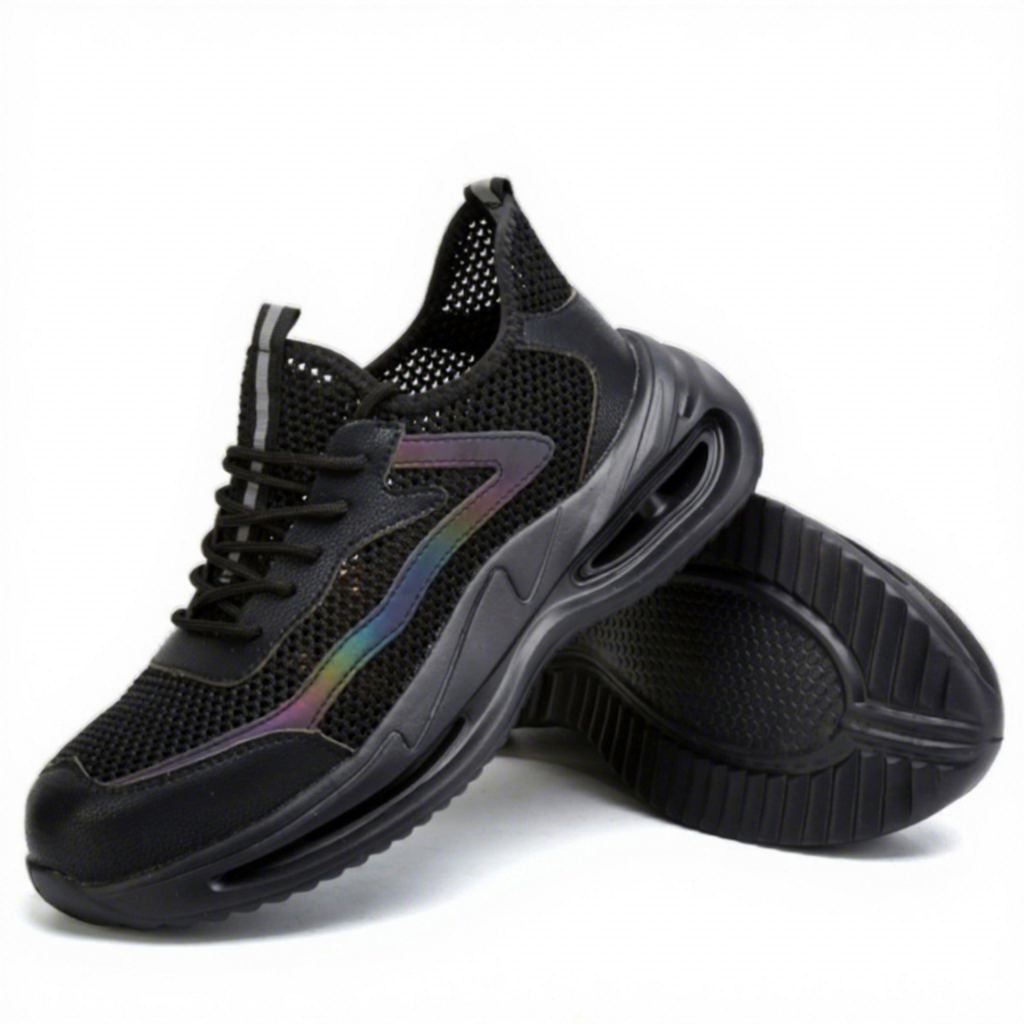
All-Season Breathable Mesh Safety Shoes Anti-Smash Anti-Puncture Lightweight Steel Toe Cap Men High-Density
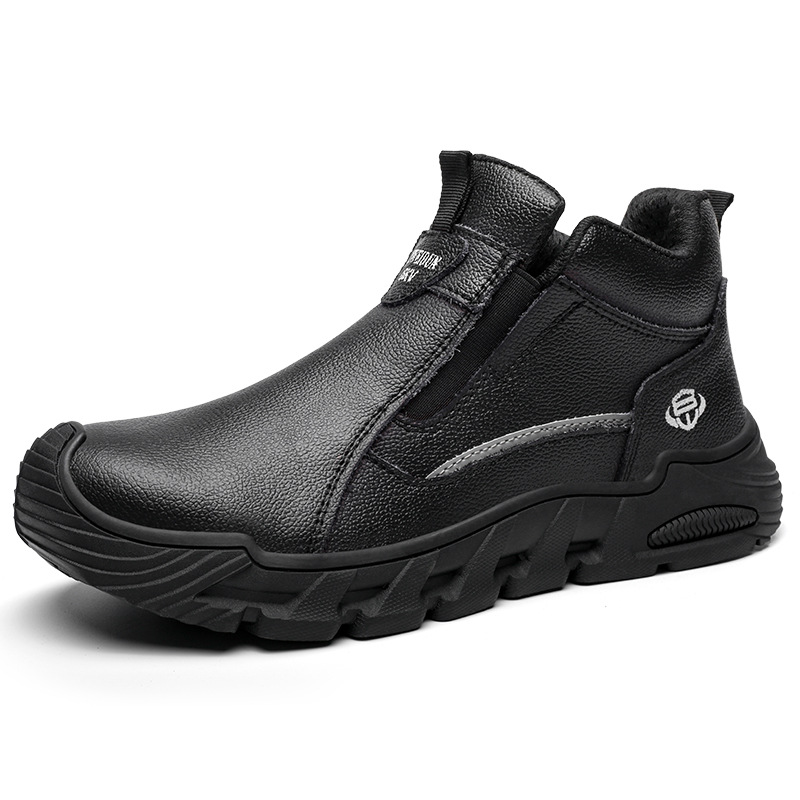
Waterproof Cowhide Upper Safety Shoes Electrician's Insulated Boots Crush-Resistant Rubber Outsole Plastic Toe Cap Men's Welding
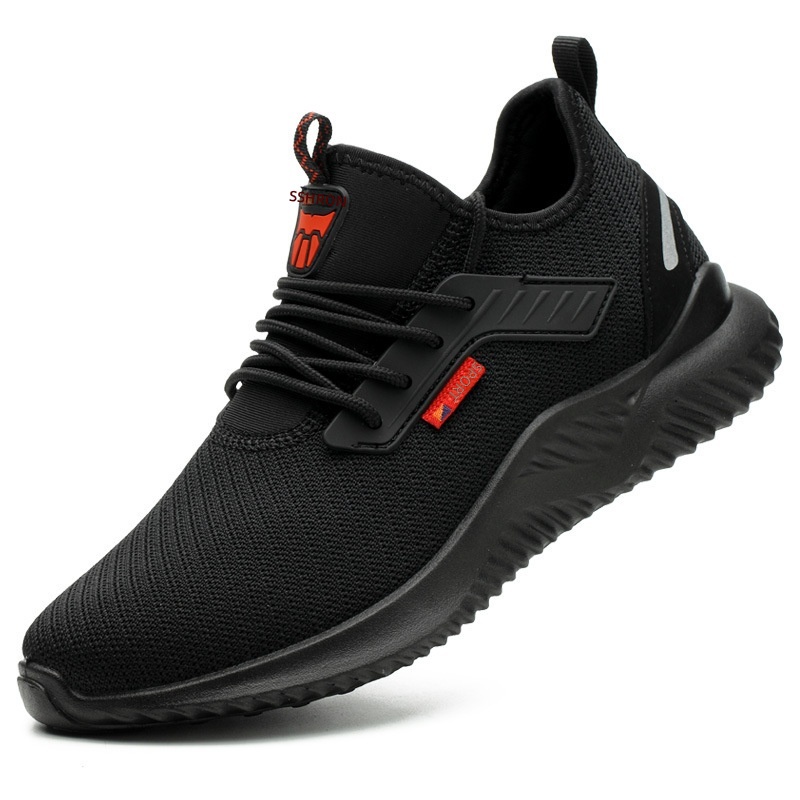
Cross-border Leather Ladle Head Toe Steel Toe Work Safety Shoes Four-season EVA Sole Mechanical Manufacturing Certified
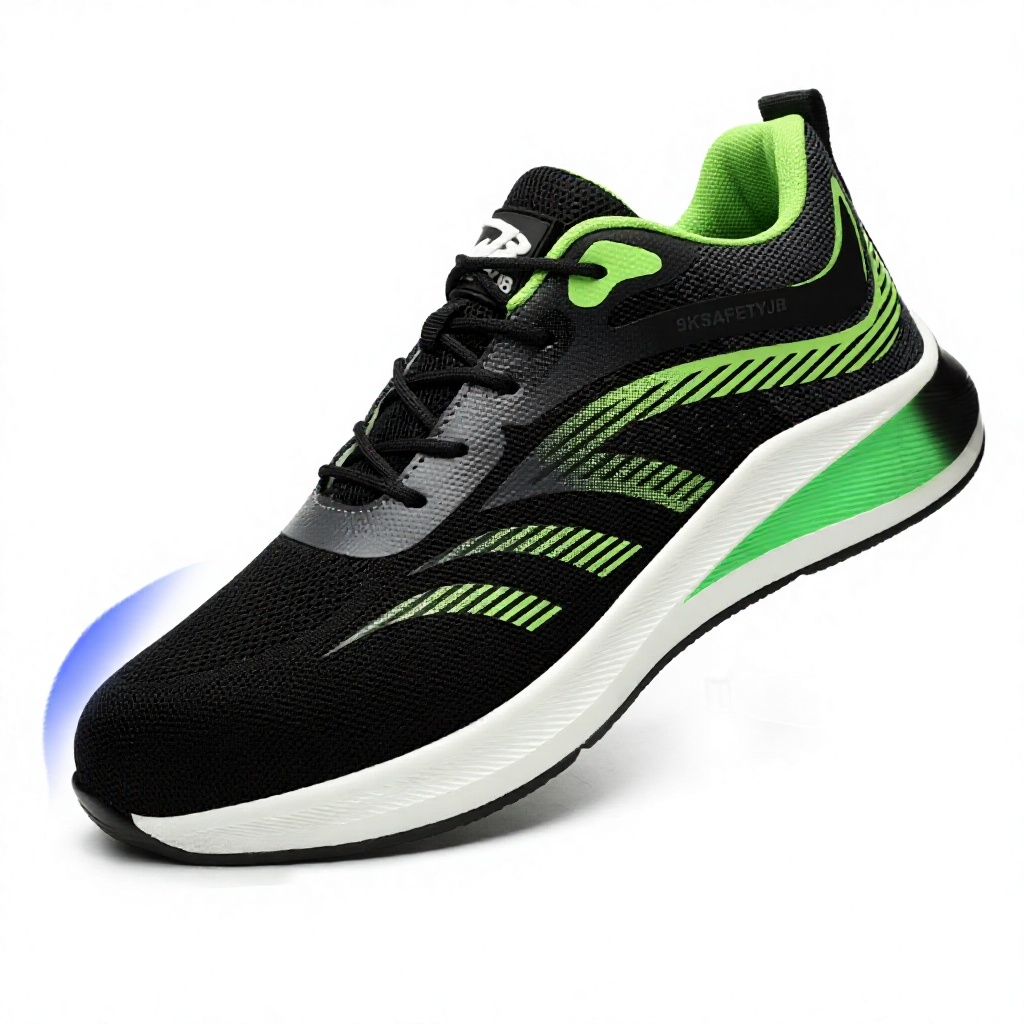
Unisex Labor Protection Safety Shoes Steel Toe Cap Breathable for Upper PU Sole Summer Work Construction Shoes
Material Science of Hydrocarbon & Oil Resistance
A comprehensive analysis of polymer density, molecular cross-linking, and anti-slip rheology in modern Personal Protective Equipment (PPE).
Sol-Gel Polymer Vulcanization
Standard industrial shoe compounds degrade rapidly when exposed to aliphatic hydrocarbons, hydraulic fluids, and crude fuels. Our factory integrates closed-cell cross-linked Nitrile Butadiene Rubber (NBR) combined with vulcanized thermoplastic polyurethanes (TPU). This chemical synthesis eliminates liquid migration into the polymer matrix, guaranteeing volume swell remains below 1.2% after 22 hours of continuous ASTM D471 IRM 903 immersion testing.
Kinetic Friction Co-efficient (SRC)
Slip-and-fall hazards on oily steel surfaces cause over 37% of factory floor lost-time injuries. We engineer tread profiles featuring multi-directional siping and self-clearing micro-channels. Siping displaces fluid film instantly, allowing the tread elements to make direct mechanical contact with the substrate. Our outsoles deliver an SRC co-efficient of friction above 0.38 against glycerol-lubricated steel, far surpassing global minimums.
Dual-Density Injection Moulding
To resolve the historic trade-off between rigid protective outsoles and worker fatigue, we employ dual-density DESMA injection lines. The outer skin utilizes high-density, abrasion-resistant, oil-impervious PU/Rubber (Shore A 65-70), while the midsole layer leverages expanded low-density PU (Shore A 45-50). This structure achieves superior energy absorption at the heel exceeding 35 Joules according to EN ISO 20344 structural protocols.
4.5M+
Pairs Annual Capacity
<0.8%
Immersion Swell Ratio
100%
In-Line Dielectric Testing
85+
Export Destination Markets
Why International EPCs and Wholesalers Choose Us
Combining decades of precision shoemaking heritage with certified traceability, vertically managed material supply, and lean export processes.
Vertically Integrated Material Synthesis
Unlike assembly-only workshops, our factory operates internal polymer compound mixing and leather tanning facilities. We control raw rubber compounding, vulcanization accelerators, and water-repellent cowhide tanning in-house. This upstream control prevents batch-to-batch chemical variance and locks in stable pricing across year-long supply agreements.
Certified Testing Laboratory
Every production lot is subjected to comprehensive destructive and non-destructive evaluations in our CNAS-accredited testing facility. Testing protocols cover 200J drop-hammer impact resistance, 15kN compression tests, 1100N puncture resistance tests on composite/steel plates, continuous flexing fatigue (150,000 cycles), and oil/acid degradation simulations.
Bespoke OEM/ODM Customization
We supply global distributors with full private-label services, including CAD upper profiling, custom laser-etched outsoles, injection-moulded composite toe profiles, dual-color injection accents, bespoke retail boxes, and multilingual instruction manuals compliant with Regulation (EU) 2016/425.
Future Procurement Trends in Oil-Resistant Safety Shoes
Anticipate regulatory shifts and material upgrades to optimize procurement cycles and secure higher market share.
Non-Metallic Composite Transitions
Global logistics hubs and offshore refineries are phasing out carbon steel toe caps and steel midsoles in favor of non-conductive, ultra-light carbon nanotube composites and ballistic aramid penetration barriers. These reduce overall weight by up to 25%, avoid triggering sensitive airport and perimeter security detectors, and offer superior thermal insulation in extreme operating climates.
Circular Polymers & Bio-Based Polyols
Environmental, Social, and Governance (ESG) guidelines across the European Union and North America are forcing brand owners to evaluate carbon lifecycle metrics. Future procurement will demand safety footwear formulated with bio-succinic acid-derived polyols and post-industrial recycled rubber outsoles that maintain EN ISO FO oil resistance thresholds without compromising environmental accountability.
Smart Ergonomics & BOA Lacing Integration
Workplace ergonomic regulations are prompting buyers to look beyond baseline compliance. Rapid wire-dial fit systems (such as BOA) are replacing traditional laces to mitigate machinery snag hazards and streamline ingress/egress. In addition, orthopedic insoles engineered with memory-recovery thermoplastic elastomeric polyurethane (E-TPU) are becoming mandatory components for high-volume enterprise tenders.
Frequently Asked Questions by Safety Shoes Importers
Practical answers covering international testing certifications, raw material specifications, minimum order parameters, and logistics.
What differentiates standard slip-resistant footwear from certified oil-resistant (FO) shoes?
Standard slip-resistant shoes are typically tested on ceramic tile lubricated with dilute soap solution (SRA). Certified oil-resistant footwear must satisfy the "FO" (Fuel Oil) standard under EN ISO 20345:2022. This requires immersing outsole samples in 2,2,4-trimethylpentane for 22 hours at 23°C. The volumetric expansion must not exceed 12%, and the hardness deviation must remain within narrow tolerances. Standard rubber outsoles swell, soften, delaminate, and lose traction when exposed to oils, whereas our specialized cross-linked NBR/PU polymers retain dimensional stability and structural density.
Can you supply dual-certified footwear for both EU and North American safety standards?
Yes. Our engineering department develops dual-certified protective lasts and safety caps that comply with both EN ISO 20345:2022 (S1P, S2, S3, S7 SRC ratings) and ASTM F2413-18 (Impact I/75, Compression C/75, Puncture PR, and Electrical Hazard EH 18,000V). We provide complete third-party test reports from notified testing bodies including Intertek, SGS, and CTC, streamlining your customs clearance and product liability validation in both markets.
How do you prevent sole delamination in high-temperature or oily chemical environments?
Delamination in harsh environments typically stems from chemical glue failure in cemented constructions. To prevent this, we utilize direct injection moulding (DESMA) technology alongside advanced polyurethane-polyurea hybrids. In this process, the molten midsole material is injected under high pressure directly onto the lasted upper, forming a permanent molecular fusion rather than relying on a separate adhesive film. For extreme mechanical conditions, we integrate 360-degree Goodyear welt stitching or sidewall stitching to guarantee permanent sole adhesion.
What are your standard Minimum Order Quantities (MOQs) and production lead times?
For custom OEM/ODM production runs requiring customized branding, personalized outsoles, and private label packaging, our baseline MOQ starts at 500 to 1,000 pairs per style across an assortment of sizes. For standard in-stock designs with minor branding adjustments, we support trial programs starting at 200 pairs. Regular container-load production cycles range between 30 and 45 days after tech-pack sign-off and deposit receipt.
Which Incoterms and international trade logistics processes do you support?
We routinely manage export contracts under FOB (Ningbo, Shanghai, Qingdao, Shenzhen), CIF, CFR, and DAP terms. For clients requiring end-to-end support, we provide full DDP (Delivered Duty Paid) shipping solutions across Europe, North America, the Middle East, and Southeast Asia. Our export documentation includes verified Certificate of Origin (Form A, Form E, CO), third-party lab inspection certificates, and MSDS chemical declarations for customs audits.
Request Engineering Datasheets & Wholesale Factory Quotations
Connect directly with our technical footwear manufacturing specialists. We provide rapid material validation, custom CAD rendering, sample prototypes, and volume factory-direct price structures tailored to your regional market.