SRC Rated
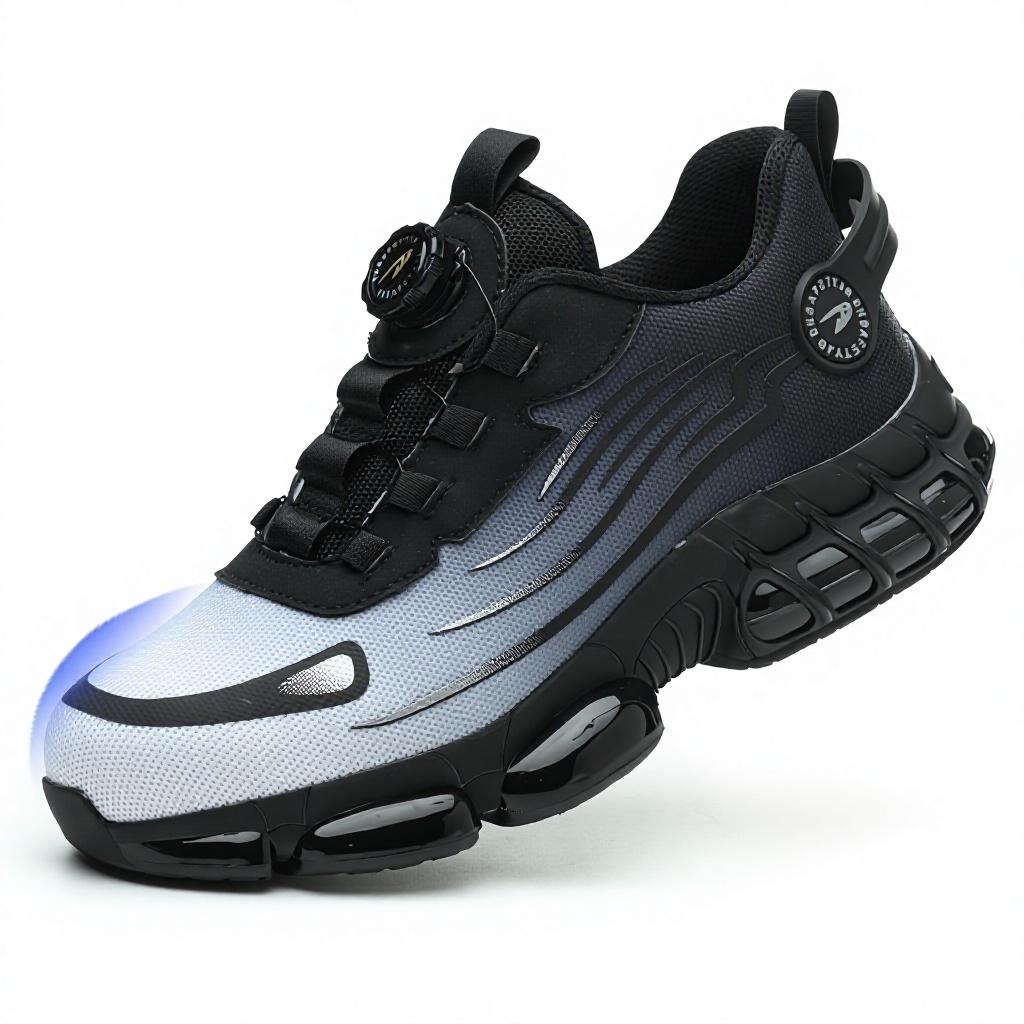
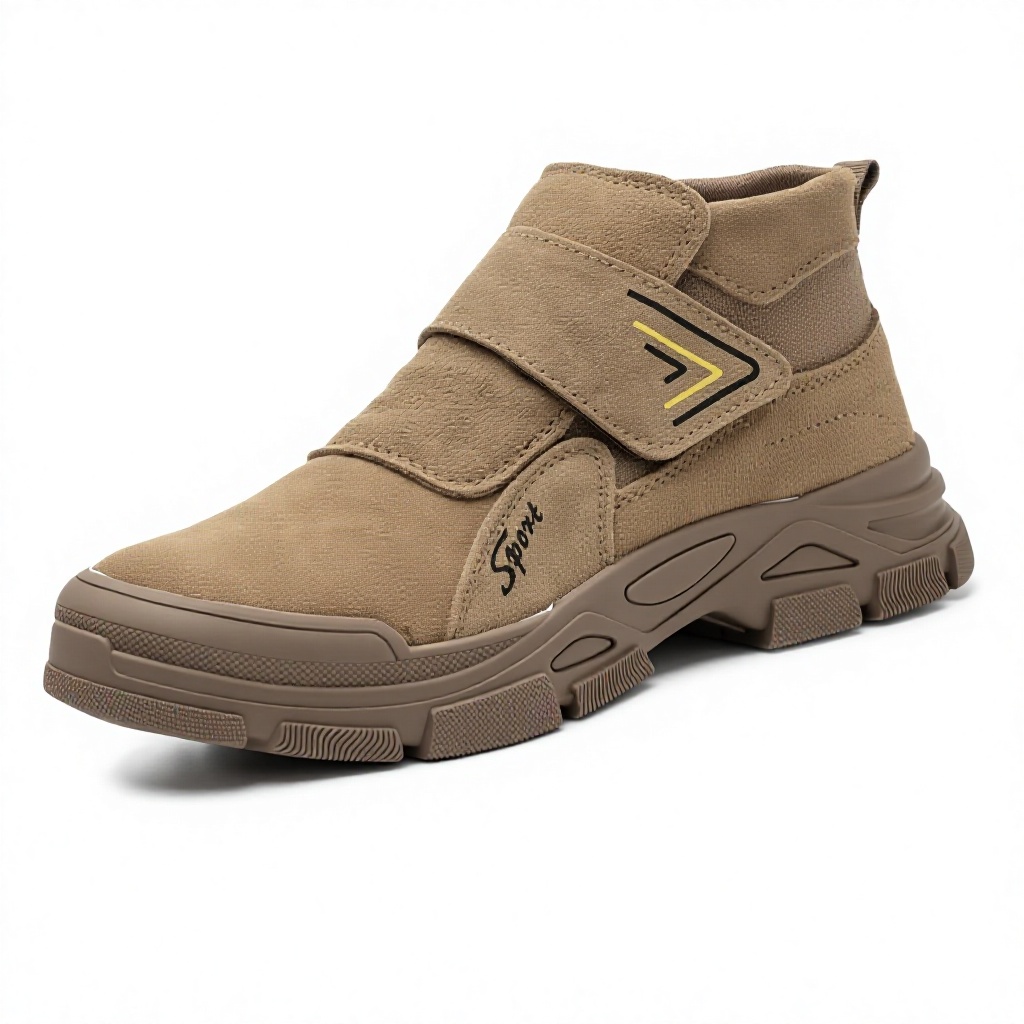
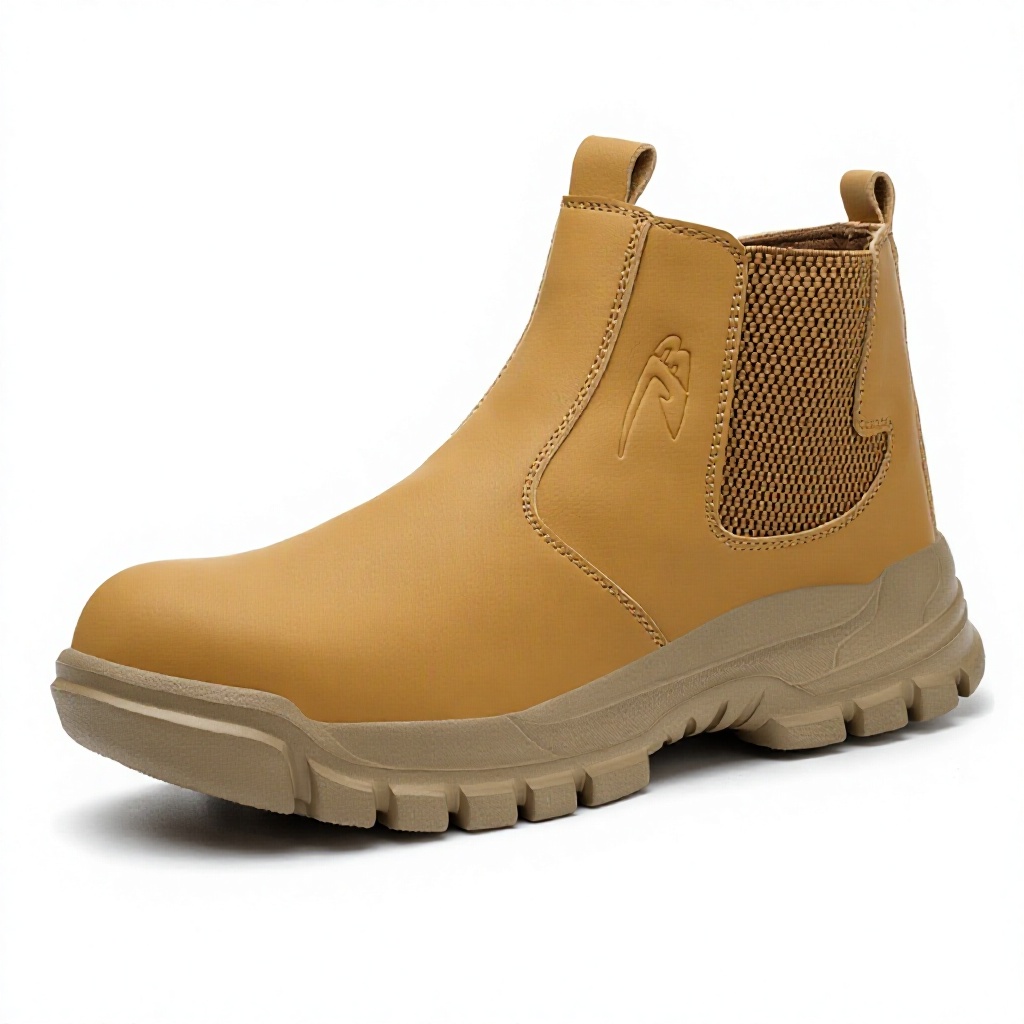
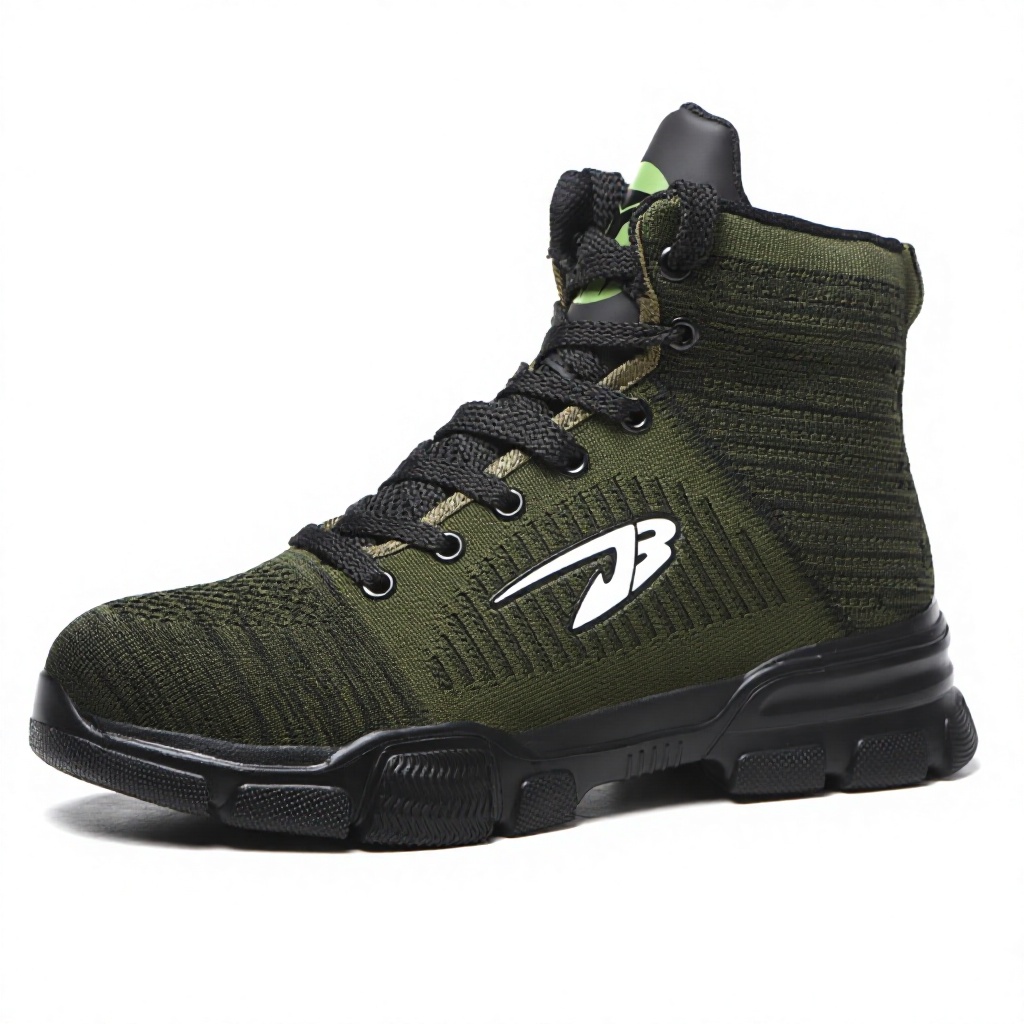
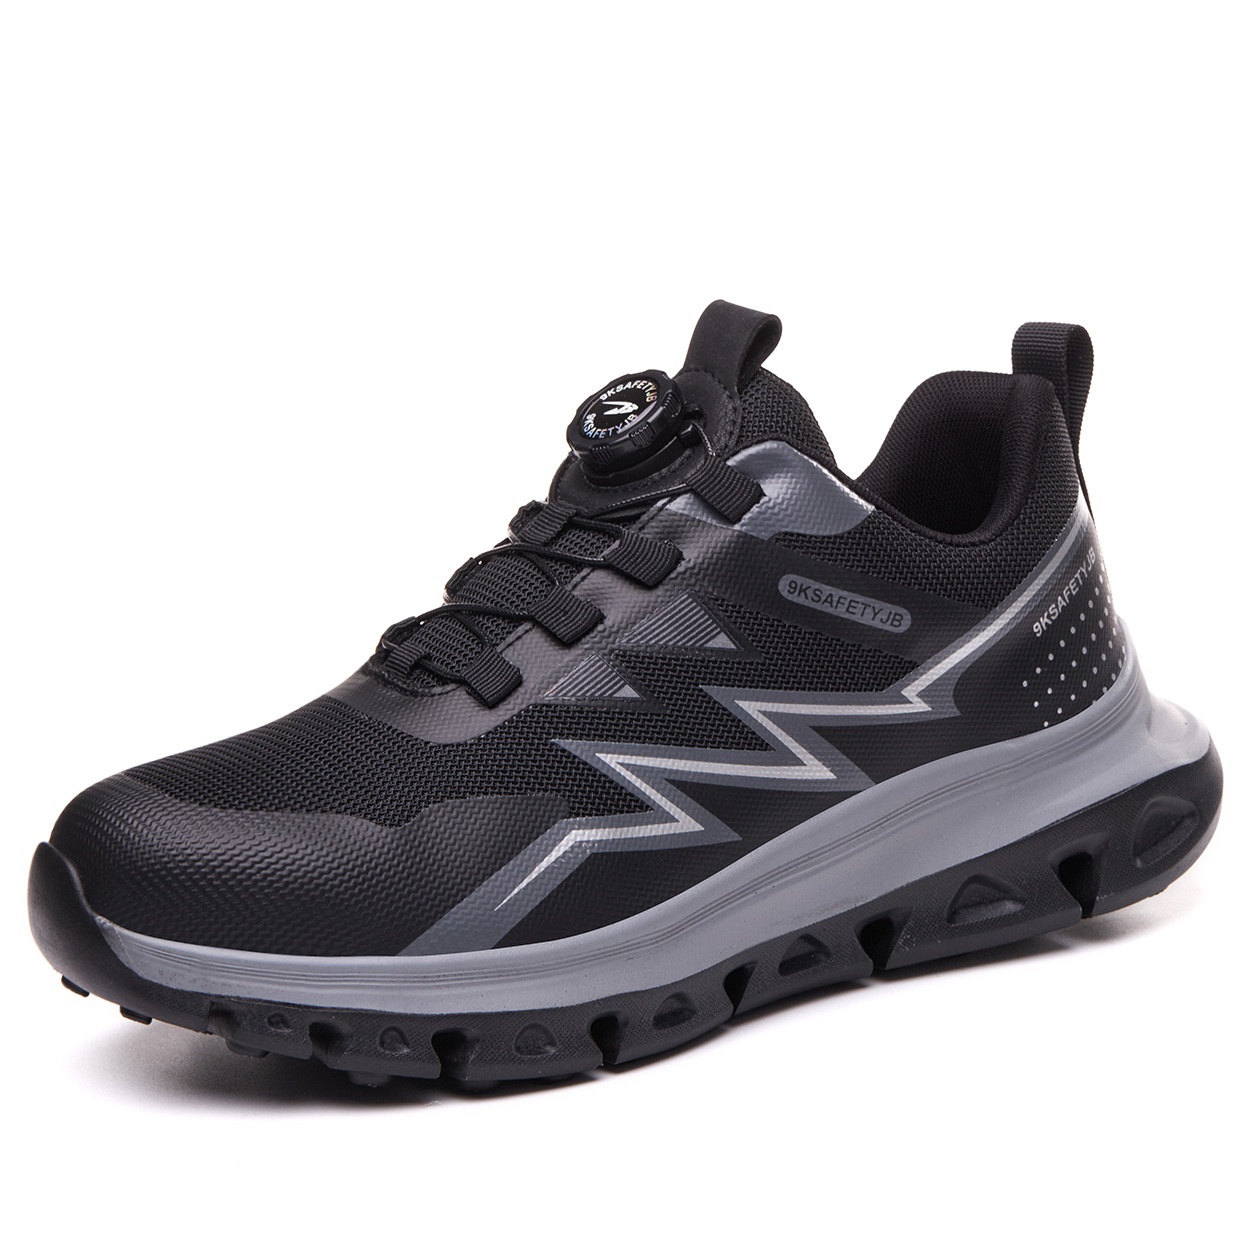
Men's Labor Protection Safety Shoes Rubber Outsole Button Closure Ladle Head Toe Puncture-Proof
- Dial Button Closure
- Rubber Outsole
- Ladle Steel Toe
Explore our export-standard safety boots engineered with anti-hydroplaning micro-treads, ladle steel toes, anti-puncture midsoles, and oil-and-acid resistant outsoles engineered for high-risk industrial environments.
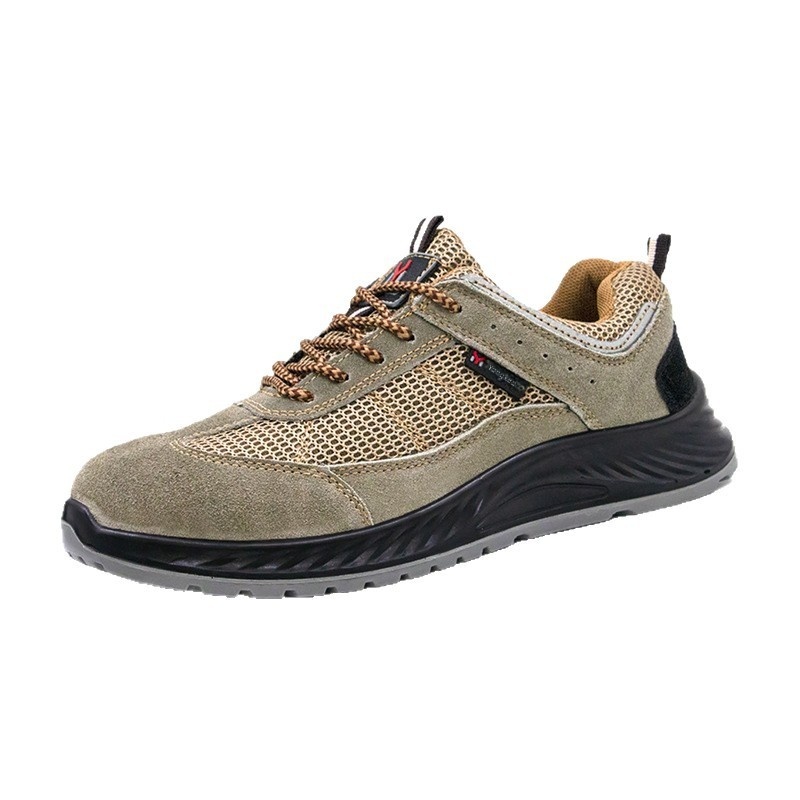
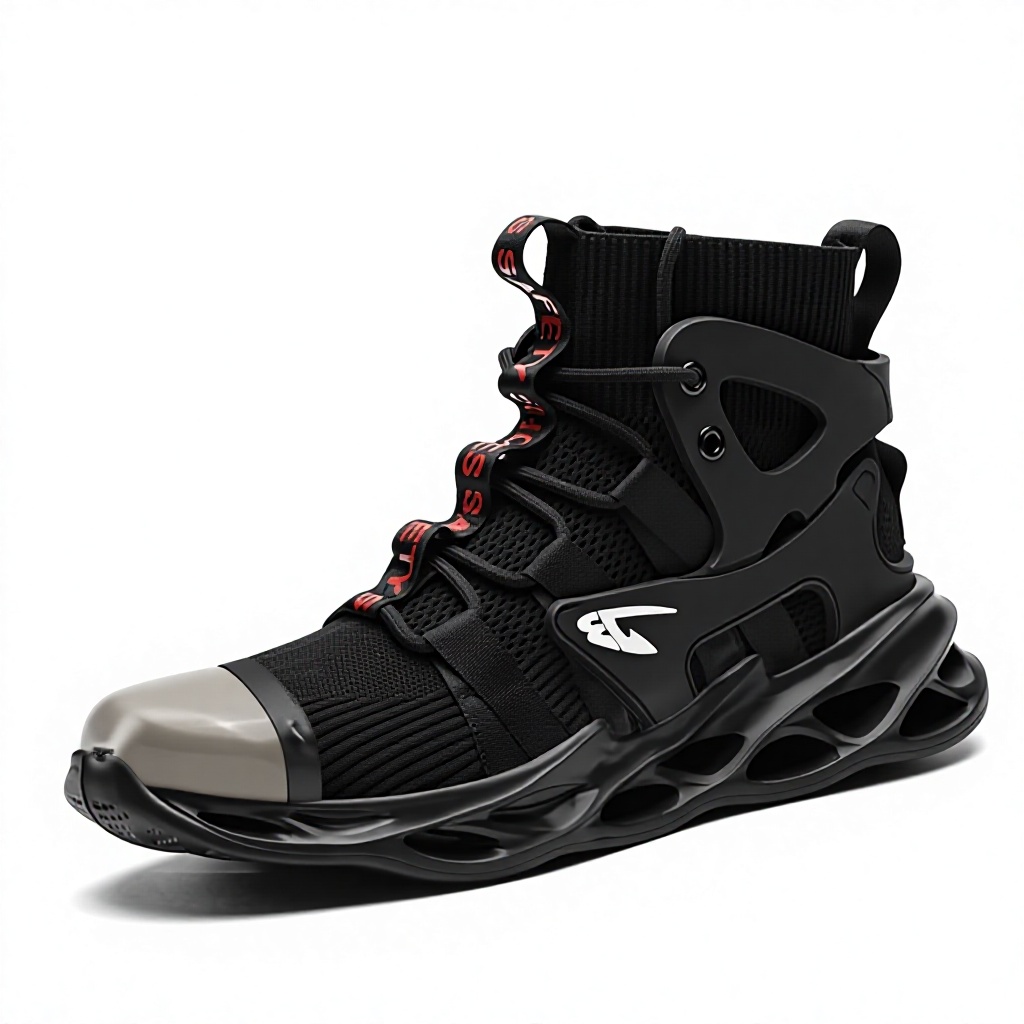
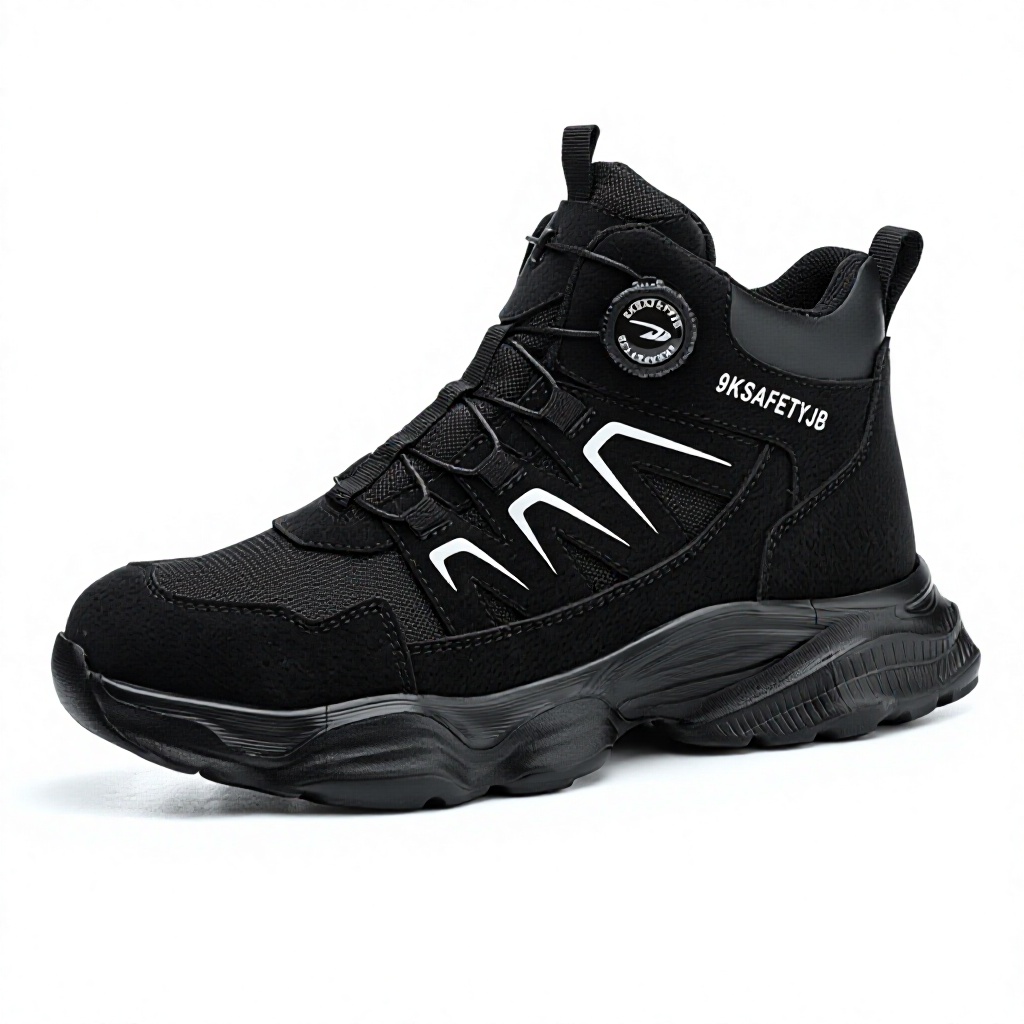
Occupational slips, trips, and falls represent over 34% of lost-workday incidents across global manufacturing, chemical processing, logistics warehousing, and commercial culinary industries. According to data monitored by OSHA (Occupational Safety and Health Administration) and the European Agency for Safety and Health at Work (EU-OSHA), the financial impact of catastrophic workplace slipping accidents exceeds $15 billion annually in North America alone. Selecting an elite slip resistant shoes manufacturer and exporter requires understanding not merely surface aesthetics, but the rigorous tribological physics governing solid-liquid boundary interaction.
True slip-resistance is quantified by the Coefficient of Friction (COF), defined as the ratio between the maximum force resisting horizontal motion and the normal force pressing two surfaces together ($μ = F_f / F_n$). Under dry ambient conditions, achieving a high COF is relatively straightforward. However, when hydrocarbons, animal fats, industrial cutting coolants, soapy water, or fine particulates saturate a polished concrete, quarry tile, or epoxy substrate, standard work footwear suffers from hydrodynamic lubrication—more commonly known as hydroplaning.
The micro-contact area of the outsole relies on dynamic mechanical dissipation. By tailoring the ratio of natural rubber (NR) and carboxylated nitrile butadiene rubber (XNBR), outsoles attain an ideal glass transition temperature (Tg) between -25°C and -40°C, delivering optimal surface wetting without excessive abrasive wear.
Liquid films as thin as 0.05 mm trigger sudden traction loss. Advanced exporters utilize laser-cut razor siping (0.4mm wide channels) structured in multi-directional herringbone patterns. These micro-capillaries evacuate fluid laterally within 15 milliseconds of heel impact, preventing fluid entrapment.
Compound stiffness determines mechanical interlock. A compound that is too rigid (Shore A > 68) skims over fluid crests; a compound that is too soft (Shore A < 50) deforms prematurely and tears under shear stress. Tier-1 manufacturers standardize on 58–62 Shore A vulcanized rubber blends.
Modern EN ISO 20345:2022 standards have phased out the outdated SRA, SRB, and SRC terminology in favor of the modernized SR designation, which requires testing on ceramic tile contaminated with sodium lauryl sulfate (glycerol and detergent mix) at heel angles of 7 degrees. Footwear exporters operating at international scale must validate continuous compliance with both EN ISO 20345:2022 SR and the rigorous North American ASTM F3445-21 Standard Specification for Slip Resistance, requiring minimum wet and dry COF values of 0.40 tested via ASTM F2913 force-plate machines.
B2B procurement managers, national retail brands, and industrial PPE distributors navigate a highly consolidated yet disparate landscape of slip resistant footwear producers. Evaluating top-tier suppliers necessitates auditing internal compound compounding facilities, injection tooling mastery, laboratory accreditations, and geopolitical export versatility. Below is an analytical review of the operational benchmarks defining the industry's top 10 manufacturing clusters worldwide.
| Manufacturer Cluster / Origin | Primary Technical Specialty | Proprietary Traction Tech | Export Compliance | Procurement Suitability |
|---|---|---|---|---|
| East China Hub (Zhejiang/Jiangsu) | Automated PU/Rubber DESMA Injection | Dual-Compound Hydro-Sipe Matrix | ASTM F3445 / CE SR | High-Volume OEM/ODM, Retail Brands, EPCs |
| South China Coastal Hub (Guangdong) | Athletic Safety Cross-over, Microfiber Flyknit | EVA/Nitrile Supercritical Foamed Soles | CE EN ISO 20345 / AS/NZS | Lightweight Architectural & Logistics Crews |
| Northern Vietnam Industrial Belt | Vulcanized Work Boots & Waterproof Leather | Aggressive Cleated Deep-Lug Outsoles | ASTM / CSA Certified | North American Heavy Mining & Construction |
| Central Mexico (Guanajuato Region) | Goodyear Welted Anti-Slip Work Boots | Nitrile Rubber Oil-Resistant Blends | ASTM F2413 / NOM-113 | Nearshore US Oil, Gas & Refining Sector |
| Western India (Agra/Chennai Clusters) | Heavy Grain Buffalo Leather Safety Footwear | Mono/Dual Density PU Outsoles | IS 15298 / CE Certified | Cost-Effective Institutional & Municipal Tenders |
| Southern Italy / Portugal Corridor | HACCP Culinary & Cleanroom Anti-Slip Clogs | Self-Cleaning Micro-Cellular PU | EN ISO 20347 SR | Food Prep, Hospitals & Pharmaceutical Plants |
| Central European Specialists (Germany/Czech) | Robotic Direct Soling & Ergonomic Lasting | Cold-Resistant Rubber-TPU Hybrid Soles | EN ISO 20345 / DGUV 112 | High-End Western European Manufacturing |
| Indonesian Footwear Corridor (Java) | Global Brand Contract Manufacturing | Multi-Density Injection Molded Sipes | ASTM / CE / JIS | Multi-Year Mega Brand Global Programs |
| Turkish Industrial Zone (Izmir/Istanbul) | Direct Injected PU-Rubber High-Ankle Boots | Acid-Proof Nitrile Vulcanization | CE / UKCA Certified | Middle East & European Heavy Metallurgy |
| Northeast USA Domestic Specialty Finishers | Specialized Military & Extreme HAZMAT Soles | Vibram/Custom Vibro-Grip Compounds | Berry Amendment / ASTM | Defense, Aerospace, Government Contracts |
While European producers excel in small-batch ergonomic styling and American domestic makers cater to regulatory defense mandates, China's coastal manufacturing infrastructure remains the undisputed global nucleus for scalable innovation, compound customization, and cost-to-performance efficiency. Top Chinese exporters possess vertical integration encompassing mold design, robotic upper stitching, computer-controlled vulcanization, and in-house SATRA-standard tribology laboratories, enabling brand partners to transition from prototype CAD drawings to high-volume commercial container shipments in under 45 days.
The safety footwear landscape is undergoing rapid technological disruption driven by sustainability directives, automated manufacturing paradigms, and worker wellness ergonomics. Procurement leaders who adapt their supply chain parameters to these five structural developments will secure distinct margin, regulatory, and safety advantages.
Traditional safety shoes relied on dense, rigid EVA or single-density PU, inducing musculoskeletal fatigue. Next-generation production integrates supercritical nitrogen-infused TPU (E-TPU), returning over 65% energy rebound per gait cycle while simultaneously dampening heel-strike vibration without sacrificing ground-plane torsional stability.
Driven by the EU Corporate Sustainability Due Diligence Directive (CSDDD), major global supply chains are phasing out petrochemical plasticizers. Exporters are formulating rubber outsoles utilizing up to 35% bio-silica derived from rice husk ash and reclaimed vulcanized ground crumb, meeting full friction standards while cutting product carbon footprint (PCF).
By 2026, safety footwear entering key European economic zones will require embedded NFC/RFID tags detailing material provenance, chemical compliance (REACH Annex XVII), and remaining outsole lifecycle tracking to optimize PPE retirement protocols before slip resistance degrades below statutory baselines.
Furthermore, the convergence of dial-based fast-lacing mechanisms (such as the micro-adjustable rotary button systems shown in our featured catalog) with breathable high-tensile woven flying mesh is transforming heavy, cumbersome labor boots into athletic-profile safety shoes. Workers across automated fulfillment centers and light assembly plants demand footwear that delivers heavy-duty S3/SR protection while maintaining the lightweight flexibility and all-day plantar arch support characteristic of elite running footwear.
As an accredited manufacturer and exporter established with comprehensive end-to-end footwear manufacturing infrastructure, our industrial facilities bridge the gap between high-precision technical engineering and aggressive commercial pricing. We do not just assemble footwear; we control the molecular integrity of the compounds and the biomechanical parameters of every silhouette.
We operate independent internal rubber internal mixers and Banbury blending units, allowing us to formulate proprietary oil-resistant, high-durometer, and low-temperature anti-slip compounds on demand, eliminating third-party compounding markups and securing strict batch consistency.
Every design is certified by recognized third-party notified bodies including TÜV Rheinland, Intertek, and CTC. We provide complete technical files for CE EN ISO 20345:2022 (SB, S1, S1P, S2, S3, and SR ratings) as well as North American ASTM F2413-18 impact, compression, and puncture resistance.
Regional foot anthropometry varies significantly; North American feet demand wider EE/EEE toe-box perimeters, whereas European lasts require contoured insteps. We maintain over 300 regional last profiles and offer rapid 3D mold prototyping within 10 working days for customized OEM outsole tread designs.
Our automated production facilities feature DESMA rotary injection soling machines, computerized upper cutting tables, and robotic cementing cells. This high degree of automation maintains bonding delamination forces well in excess of statutory 4.0 N/mm thresholds, virtually eliminating premature outsole separation warranty claims and preserving the long-term reputation of our distributor partners.
Critical answers to complex procurement, regulatory testing, minimum order thresholds, and logistical queries encountered by safety equipment distributors, tender managers, and global footwear buyers.
Connect directly with our senior footwear engineering team to discuss wholesale price matrices, request testing documentation, or order pre-production samples customized to your national regulatory standards.