Heavy Civil & Mechanical
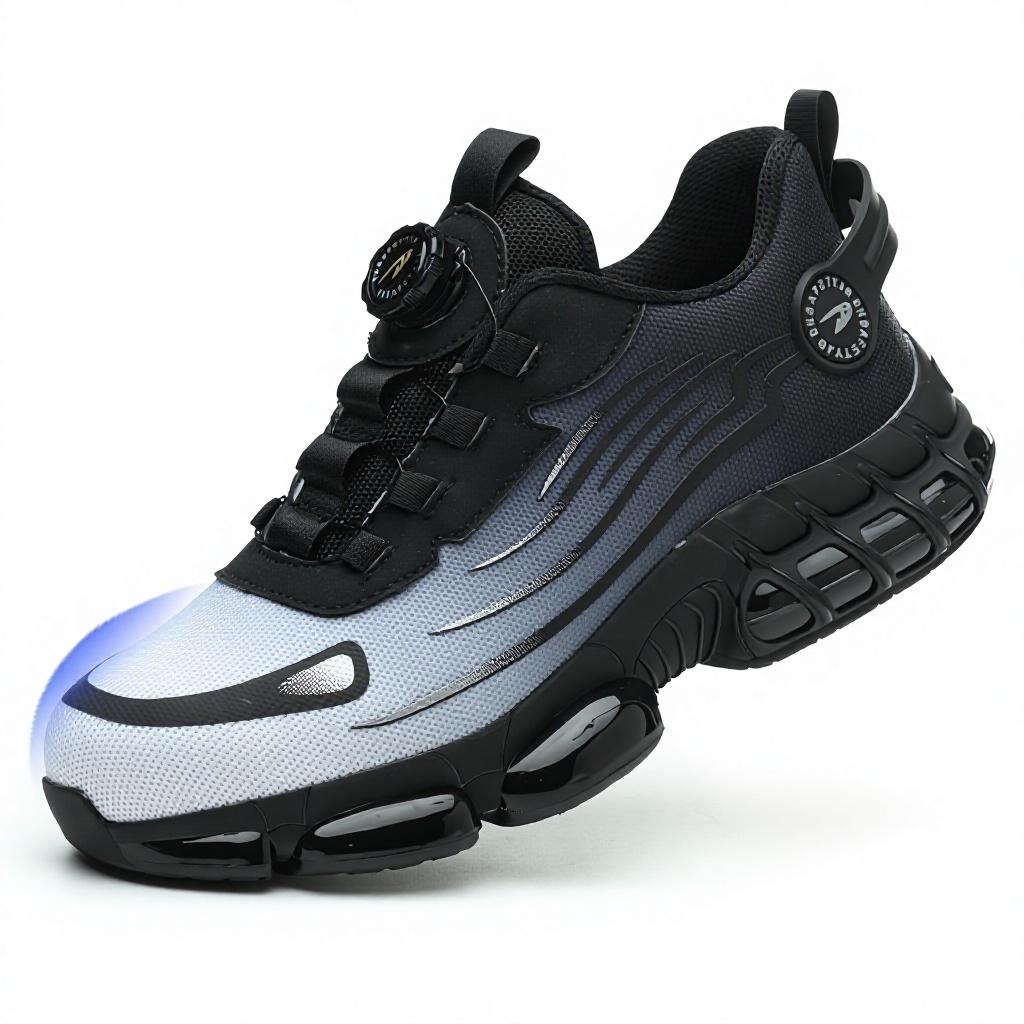
Men's Labor Protection Safety Shoes Upper Rubber Outsole Button Closure Ladle Head Toe Puncture-Proof Outdoor
Button Closure
Rubber Outsole
Ladle Head
Engineered for complex operational environments—from high-temperature mechanical assembly lines to heavy outdoor architectural sites. Compare models, inspect technical parameters, and launch sample inquiries.
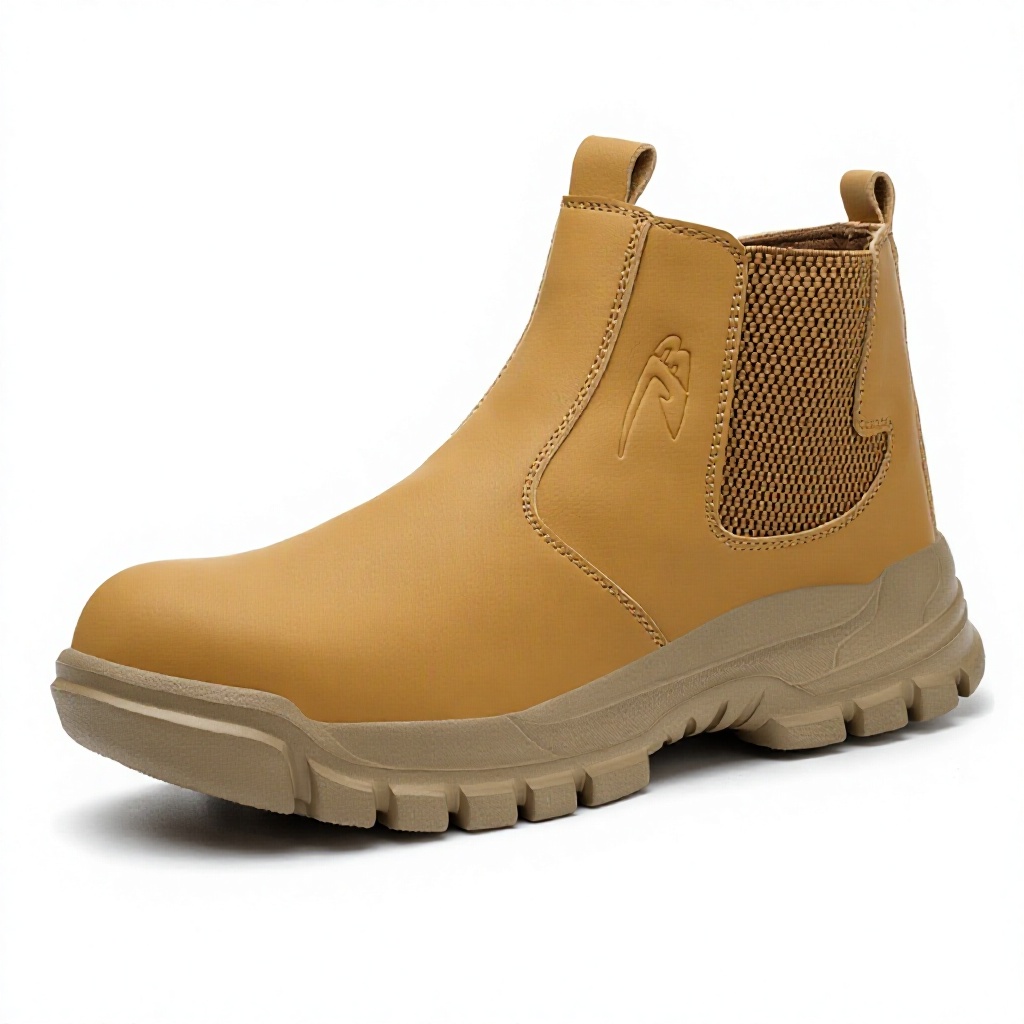
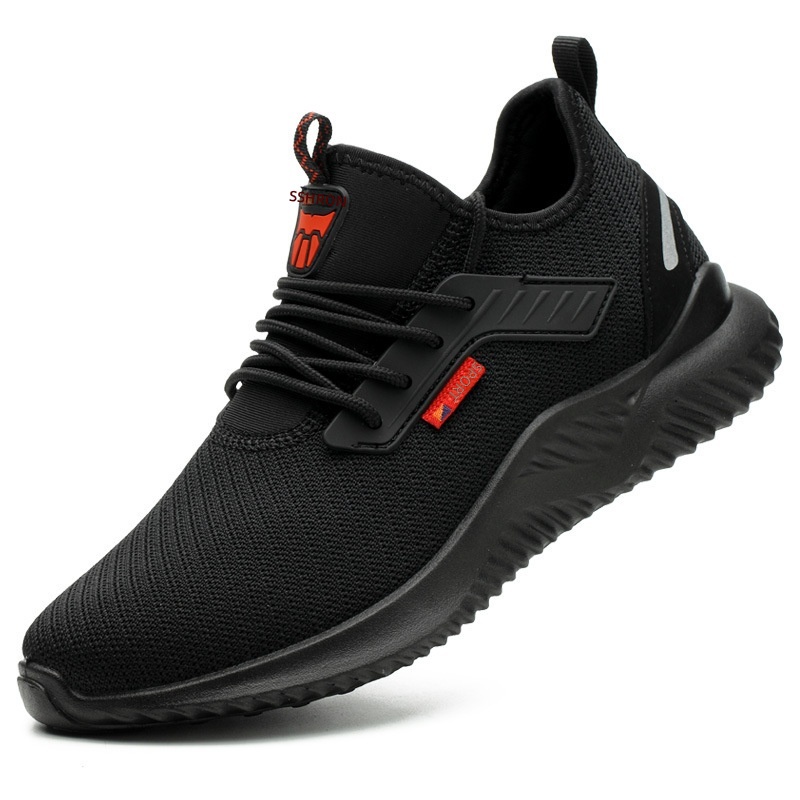
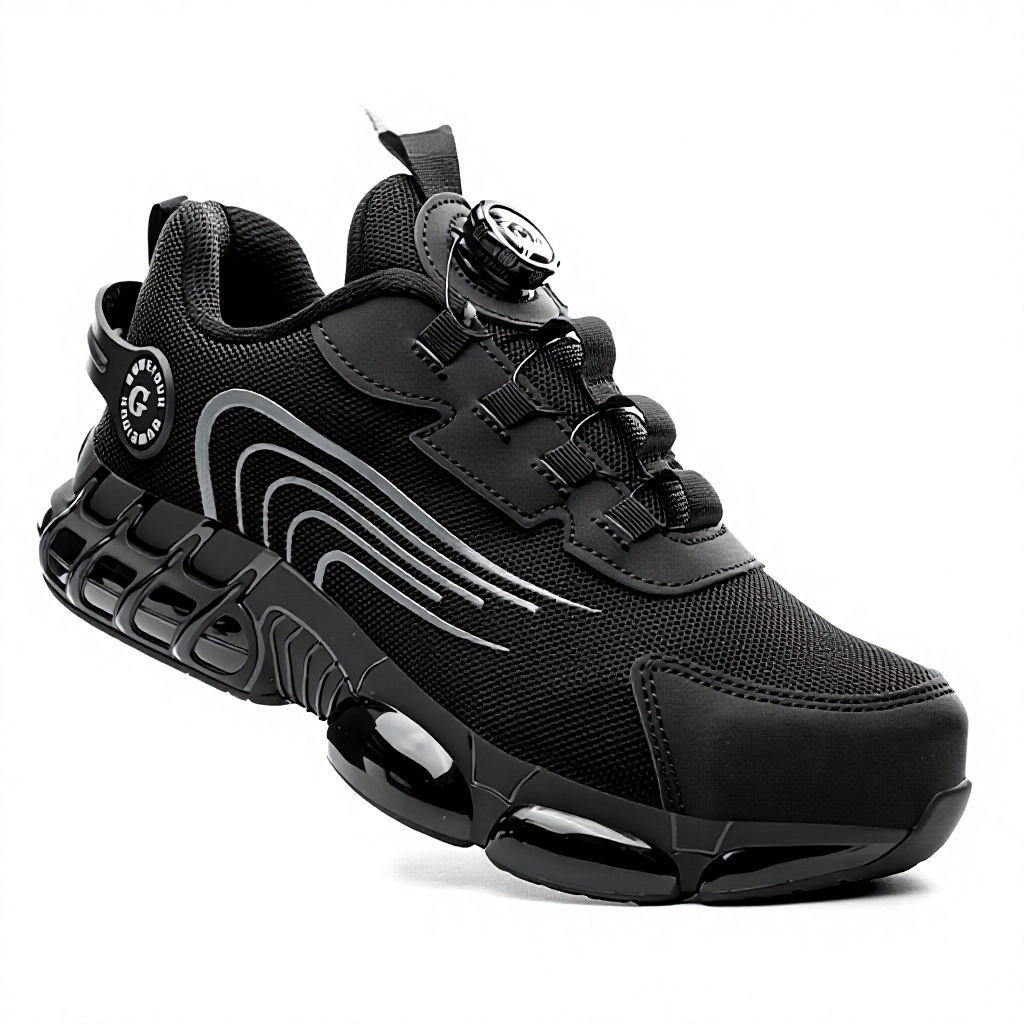
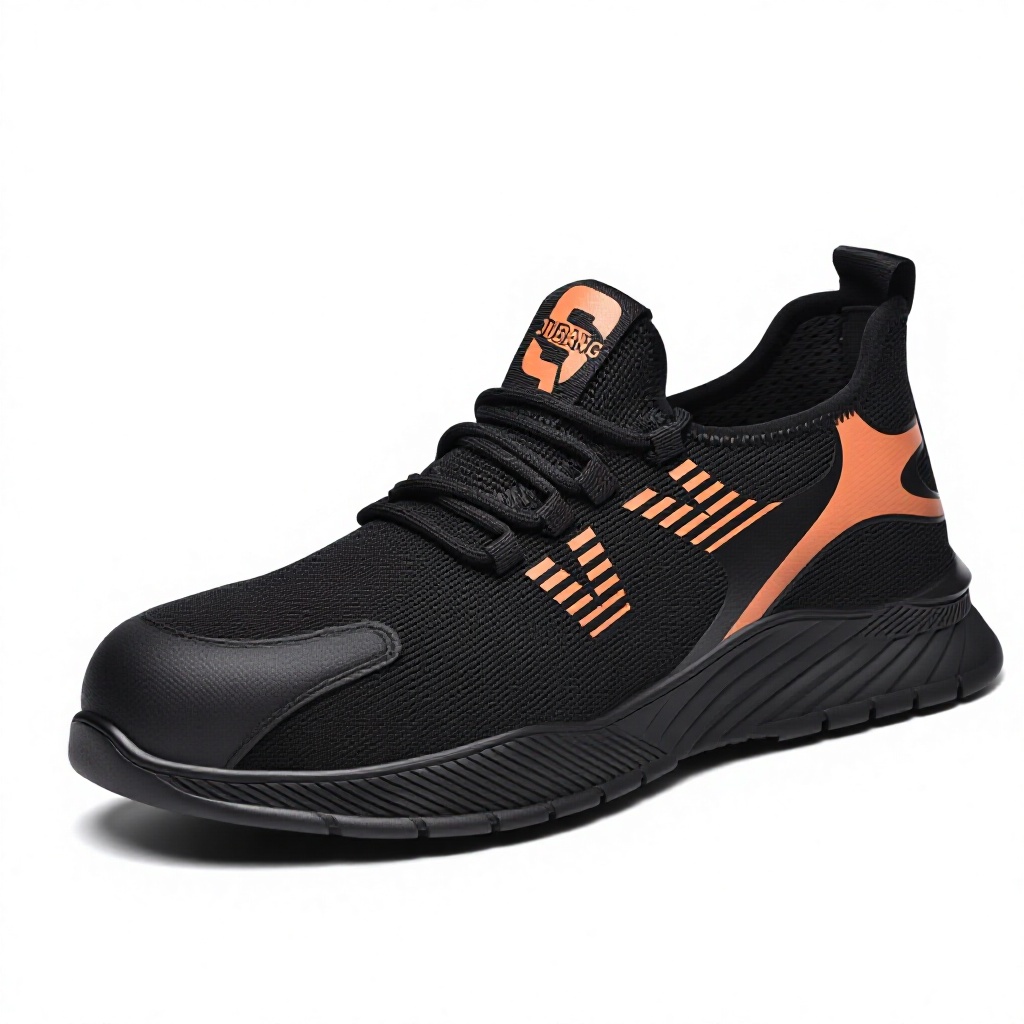
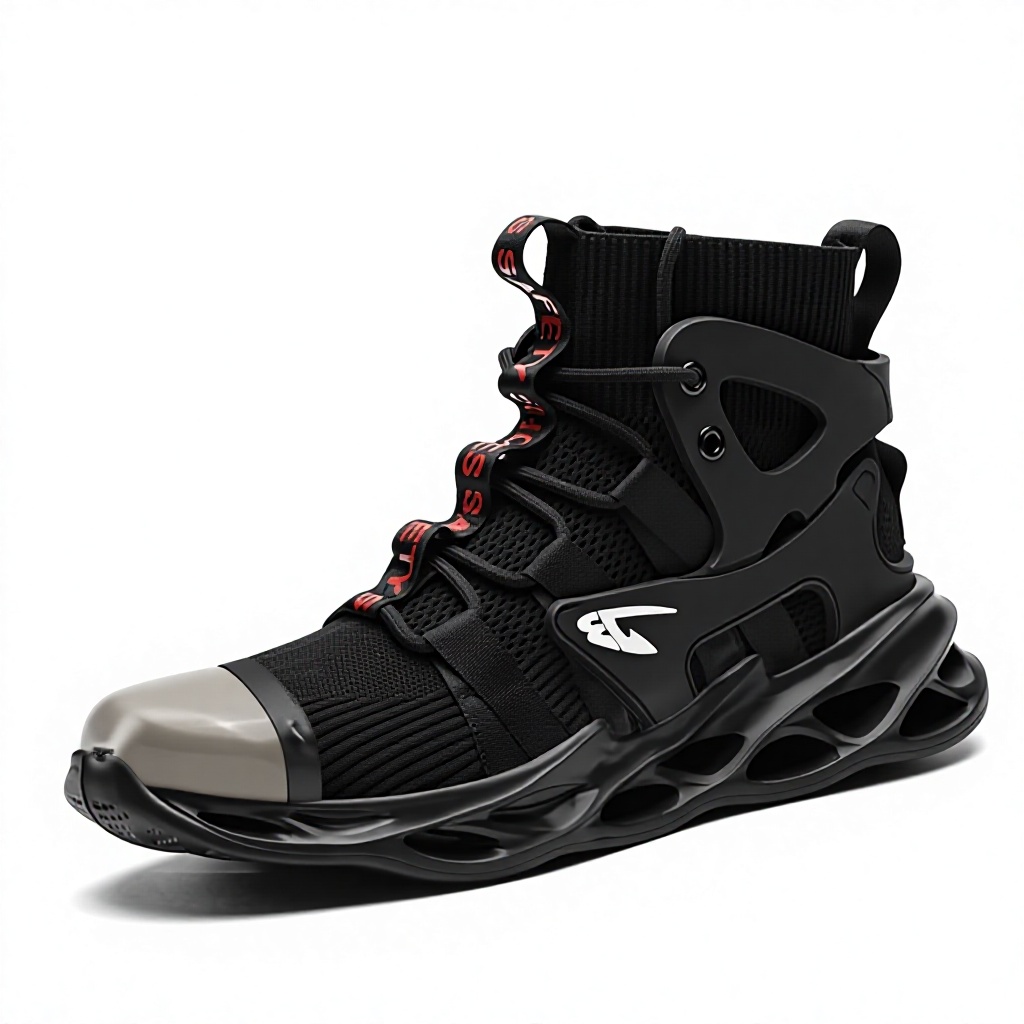
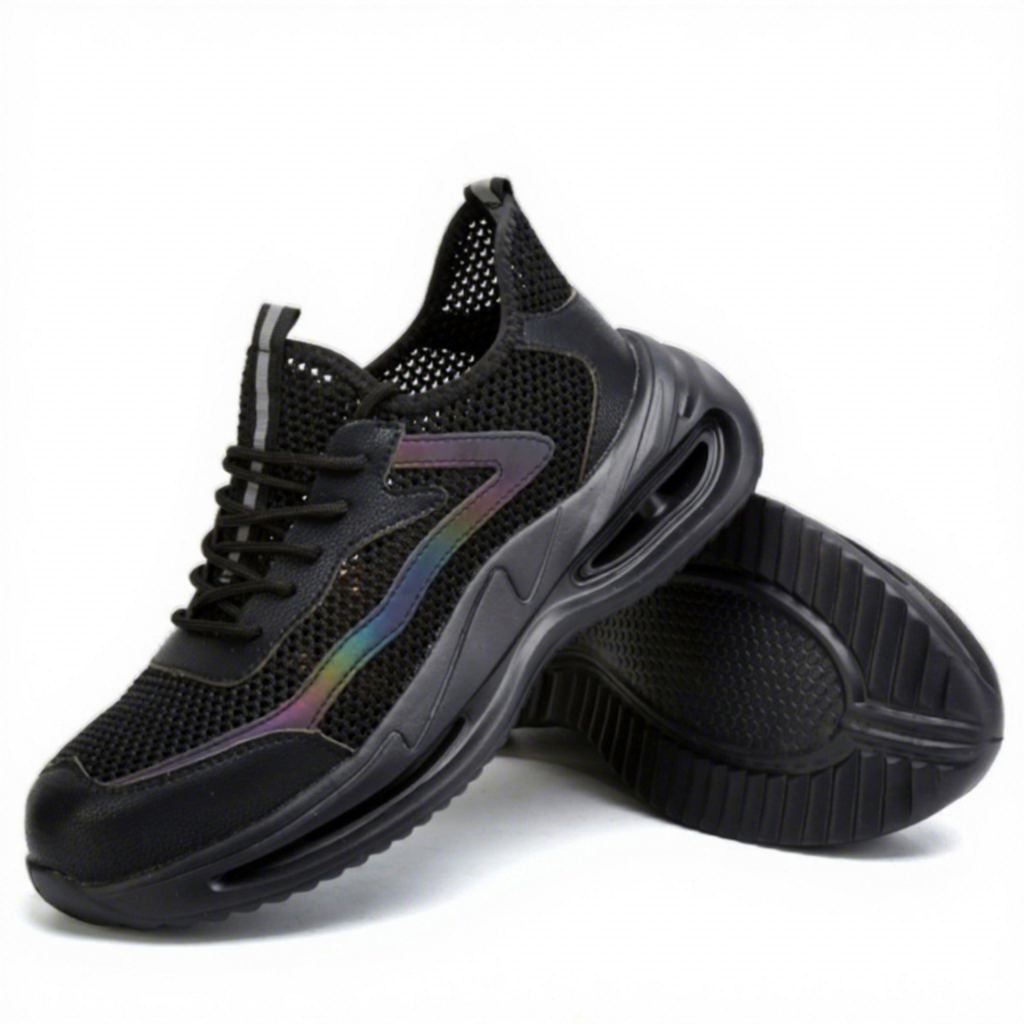
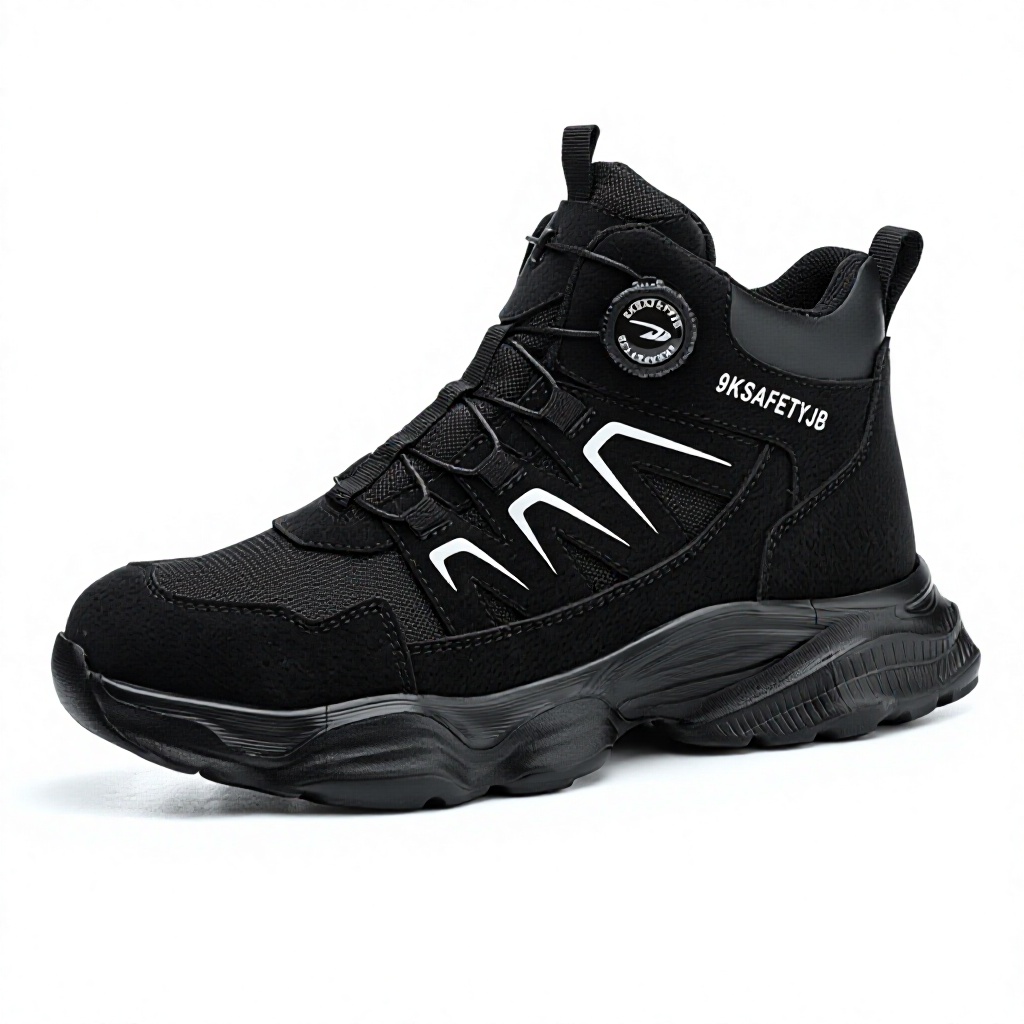
Historically, heavy industrial safety footwear enforced an unyielding technical compromise: physical impact defense (EN ISO 20345 / ASTM F2413 standards) necessitated non-porous thick leathers, rigid rubber outsoles, and dense toe caps, frequently resulting in trapped foot perspiratory moisture, thermal build-up, and plantar fatigue. Modern supply engineering has dismantled this trade-off. As a dedicated breathable safety shoes factory, our manufacturing infrastructure employs micro-porous matrix weaves, advanced high-tenacity fly-knit synthetics, and dual-density EVA/PU co-molding that allow unidirectional water-vapor evaporation while shielding the plantar and metatarsal zones from up to 200 Joules of kinetic impact and 1,100 Newtons of puncture force.
Field ergonomics demonstrates that excessive heat accumulation within safety boots triggers hyperhidrosis, which degrades dermal integrity, accelerates fungal proliferation, and reduces operative vigilance on shop floors. By adopting hyper-breathable honeycomb sandwich linings, hydrophilic vapor-permeable membrane liners, and ventilated toe-cap housings, our safety shoes stabilize the interior shoe temperature below 28°C under continuous 8-hour shift conditions. Procurement officers no longer have to reconcile safety protocol adherence with workforce physical comfort.
| Engineering Vector | Conventional Industrial Safety Boots | Our Advanced Breathable Safety Footwear |
|---|---|---|
| Upper Shell Materials | Heavy chrome-tanned split leather (non-porous) | 3D Jacquard Fly-Knit with ballistic microfiber overlays |
| Plantar Cushioning | Single-density vulcanized dense rubber | Dual-Density Phylon EVA + Energy-Return TPU cell foam |
| Vapor Transmission (WVP) | < 0.8 mg/(cm²·h) (high thermal accumulation) | > 2.5 mg/(cm²·h) certified under ISO 20344:6.6 |
| Puncture Protection | Heavy, rigid carbon steel midsoles (adds >250g) | Zero-Penetration flexible Kevlar woven composite sheet |
Analyze how international regulatory policies, decarbonization mandates, and material sciences are reshaping international footwear orders.
Enterprise buyers are transitioning from multi-vendor sourcing to qualified primary supply partners capable of handling certified anti-smash footwear alongside commercial energy equipment, optimizing freight-container cubic meters and unifying documentation.
The swift decline of traditional exposed cotton shoelaces in high-risk zones. Fast-adjusting rotational button closures and aircraft-grade steel wire cords minimize trip hazards, streamline donning time, and ensure consistent ankle immobilization across dynamic worksites.
Stringent airport, petrochemical, and electrical hazard safety demands are accelerating migration from heavy steel toe caps to lightweight fiberglass, carbon fiber, and wide-flange alloy caps that resist galvanic corrosion and non-conductive hazards.
European and American supply mandates now dictate post-consumer recycled rPET knit uppers, solvent-free hot-melt adhesives, and low-VOC polyurethane outsoles without compromising tear-resistance thresholds or chemical splash protection ratings.
Quality reliability in occupational footwear hinges upon unbroken supply chain controls. Supported by automated injection molding carousels, laser-guided material nesting, and computer-stitched upper lines, our manufacturing facility manufactures protective shoes characterized by zero batch-to-batch deviation. Every raw material roll—from hydrophobic-treated microfiber leather to anti-static conductive yarn—undergoes rigorous pre-production flex and abrasion testing.
Our internal laboratory conducts routine static compression trials, Charpy pendulum toe-box impact assessments, flexing cycles (>150,000 continuous flexes at -5°C), and Mark II slip-resistance evaluations on ceramic tile and glycerol steel beds. By leveraging locked component sourcing with Tier-1 polymer and steel cap partners, we eliminate the substandard tensile failures that plague fragmented contract manufacturers.
Full support for private-label stamping, heat-transfer rubberized logos, customized packaging geometry, customized CE mark declarations, and technical barcoding for major distributors.
Flexible international logistics execution supporting FOB, CIF, EXW, FCA, and DDP clearance with complete customs documentation (Form E, CO, MSDS, Test Summaries).
Onsite-audited operations adhering to ISO 9001 quality management guidelines, with product lines pre-tested against EN ISO 20345:2022 (S1P, S2, S3, SRC) criteria.
Direct technical feedback covering test parameters, minimum order quantities, and material classifications.
Initiate direct communication with our technical footwear engineers. Review detailed physical property dossiers, arrange custom sample testing, and optimize bulk manufacturing unit costs.
Inquire Now