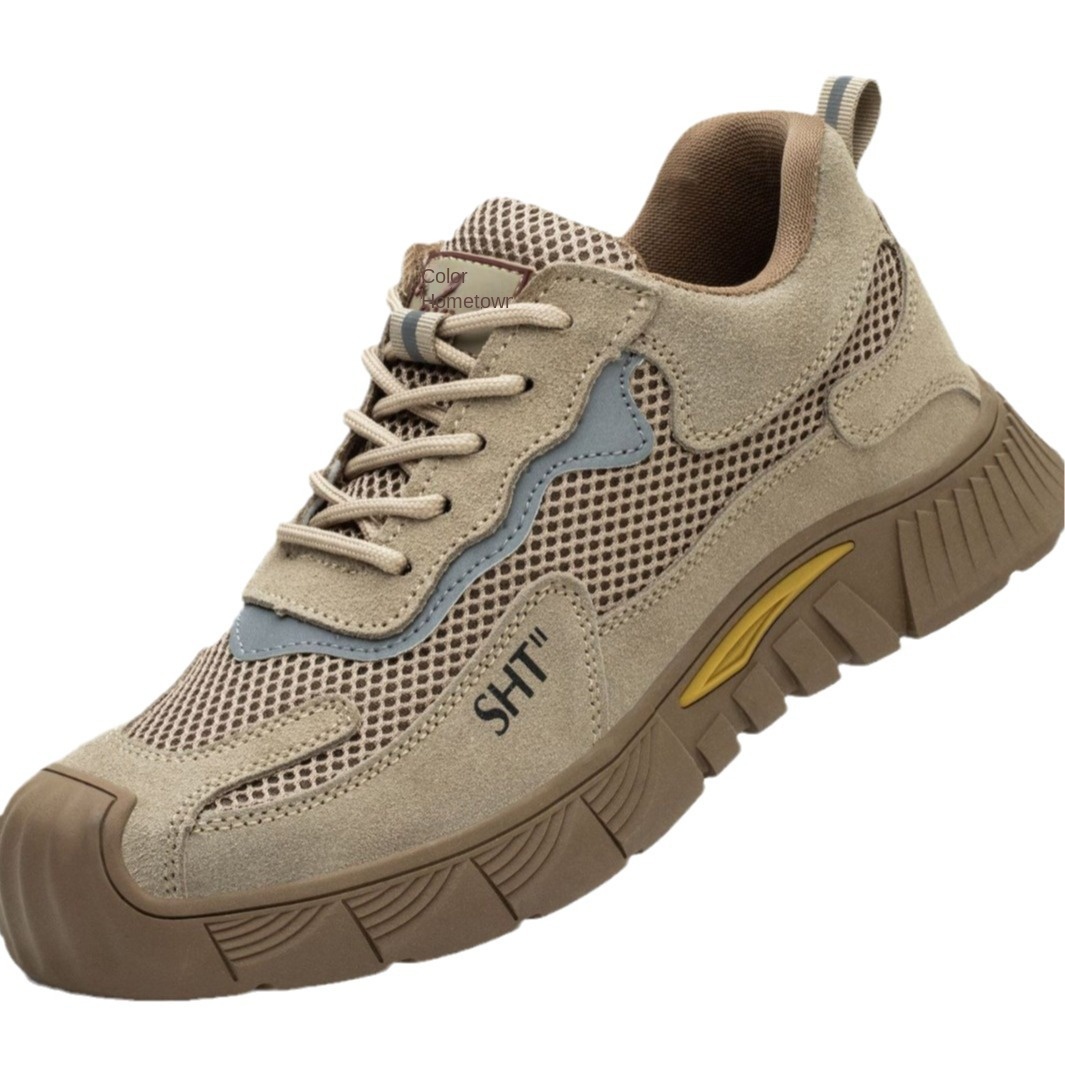
Factory Catalogue
Engineered Footwear Solutions for Tyre Plants & Heavy Fabrication
Tested against EN ISO 20345:2022 impact tolerances, high thermal vulcanization zones, puncture risks, and slip hazards present in global tire manufacturing workshops.
Warehouse & Logistics
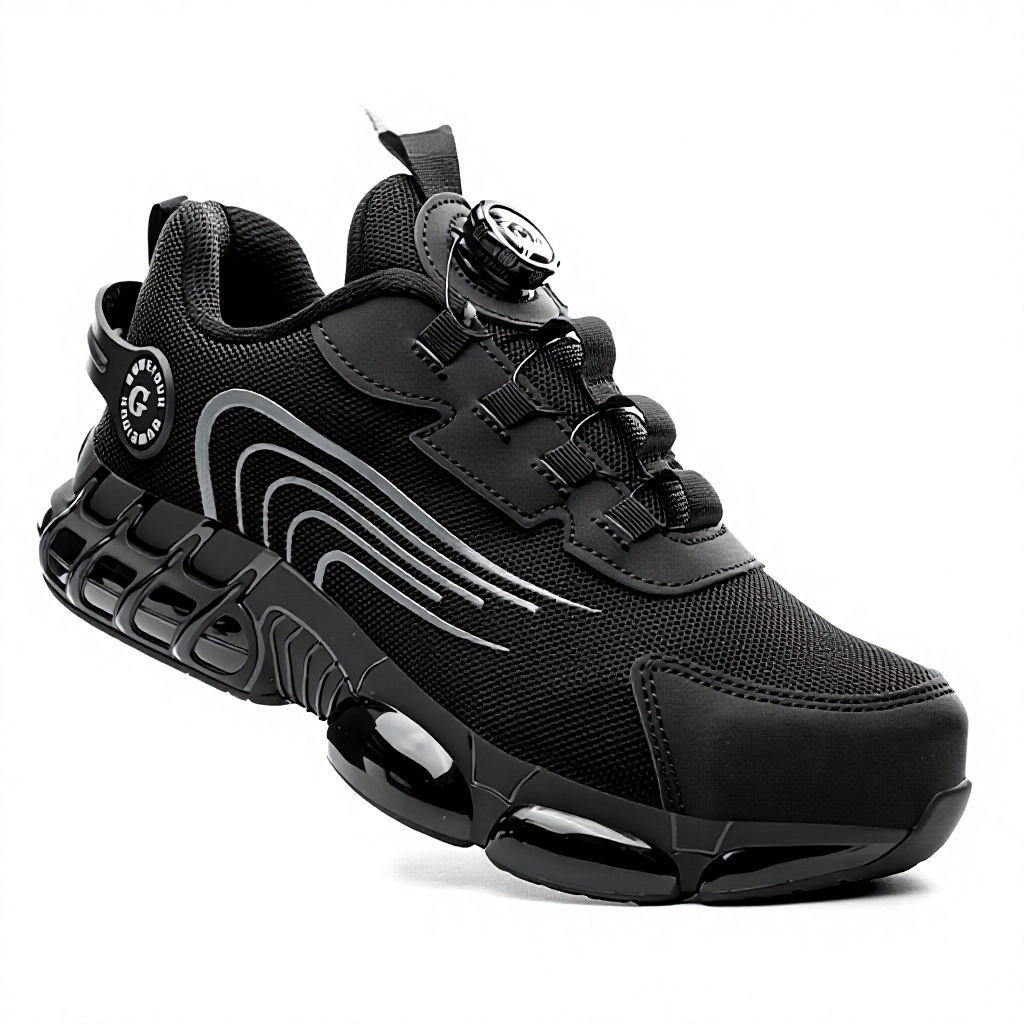
Men Steel Toe Safety Shoes Crush Resistant Puncture Proof EVA Sole
Product Specs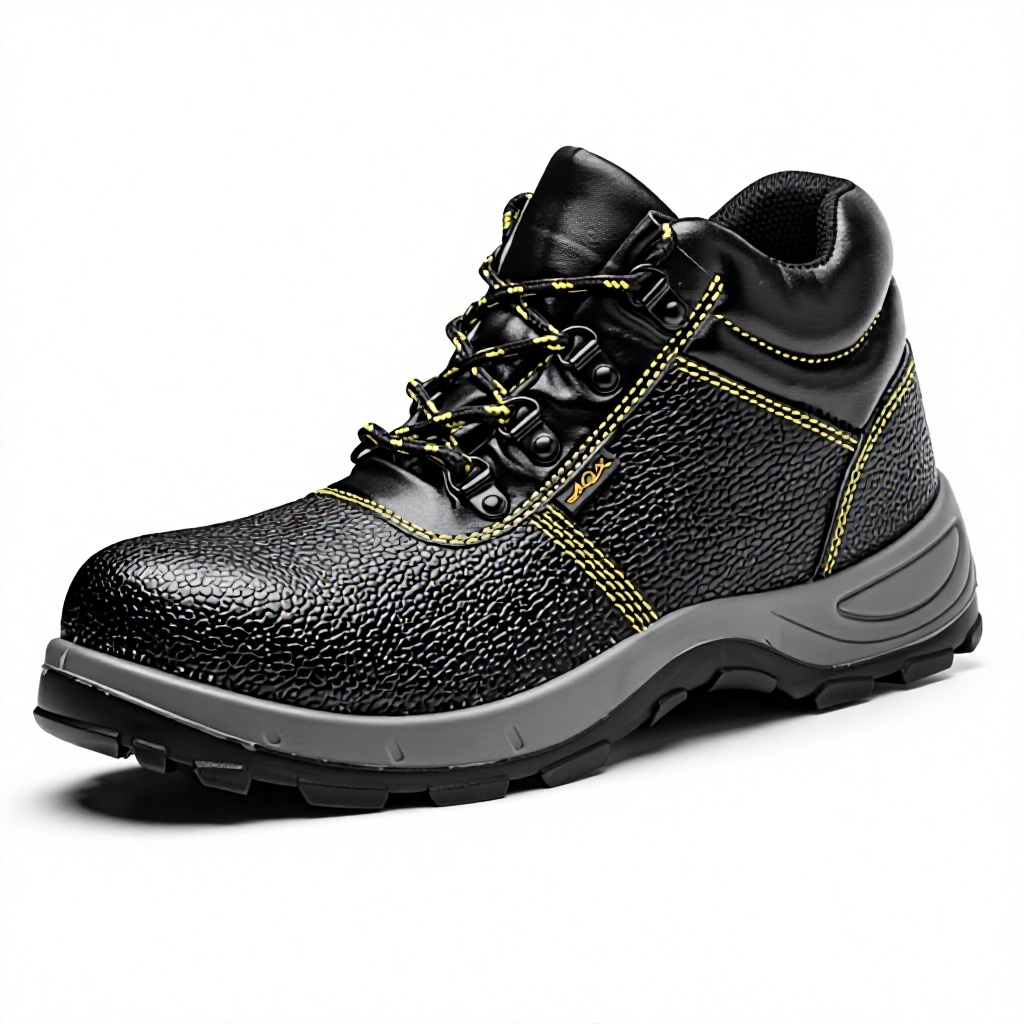
Chemical Compounding
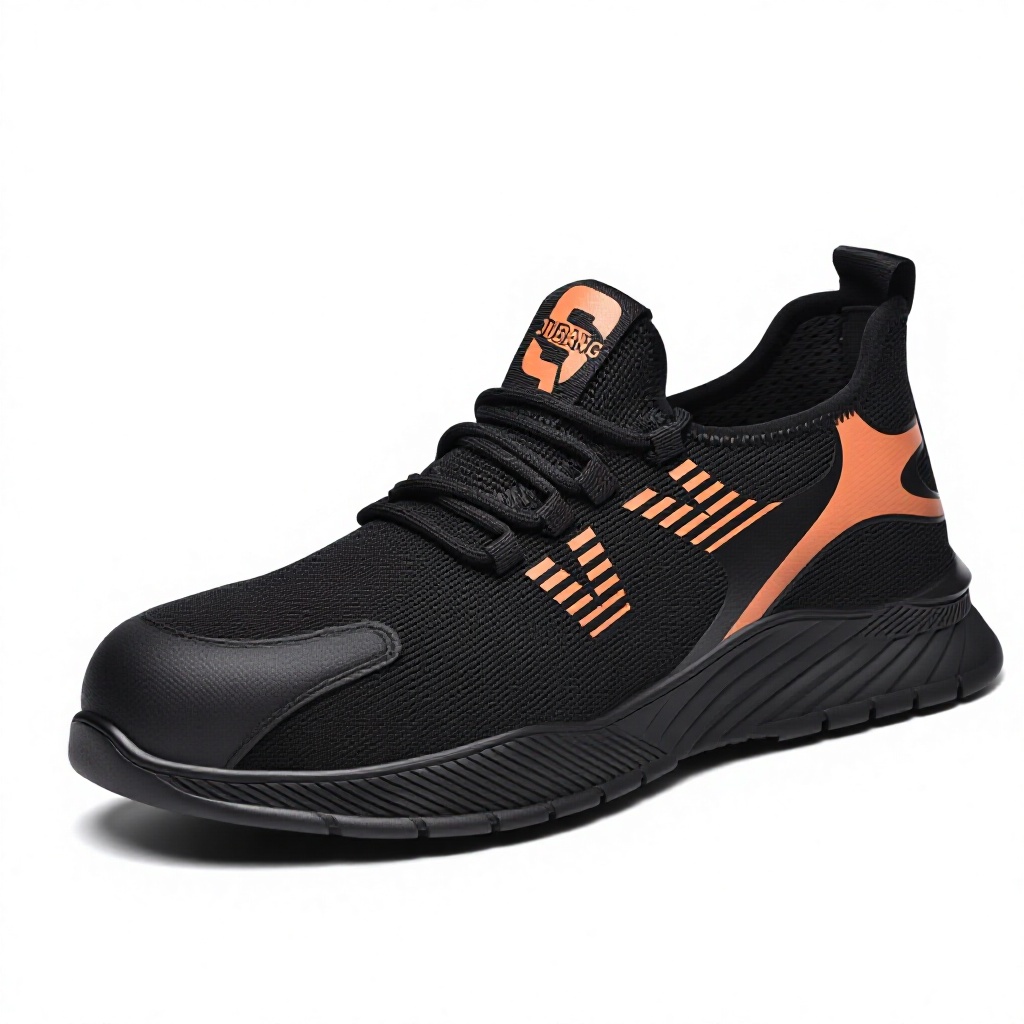
Microfiber High-Top Protective Shoes with Puncture-Proof Ladle Head
Product Specs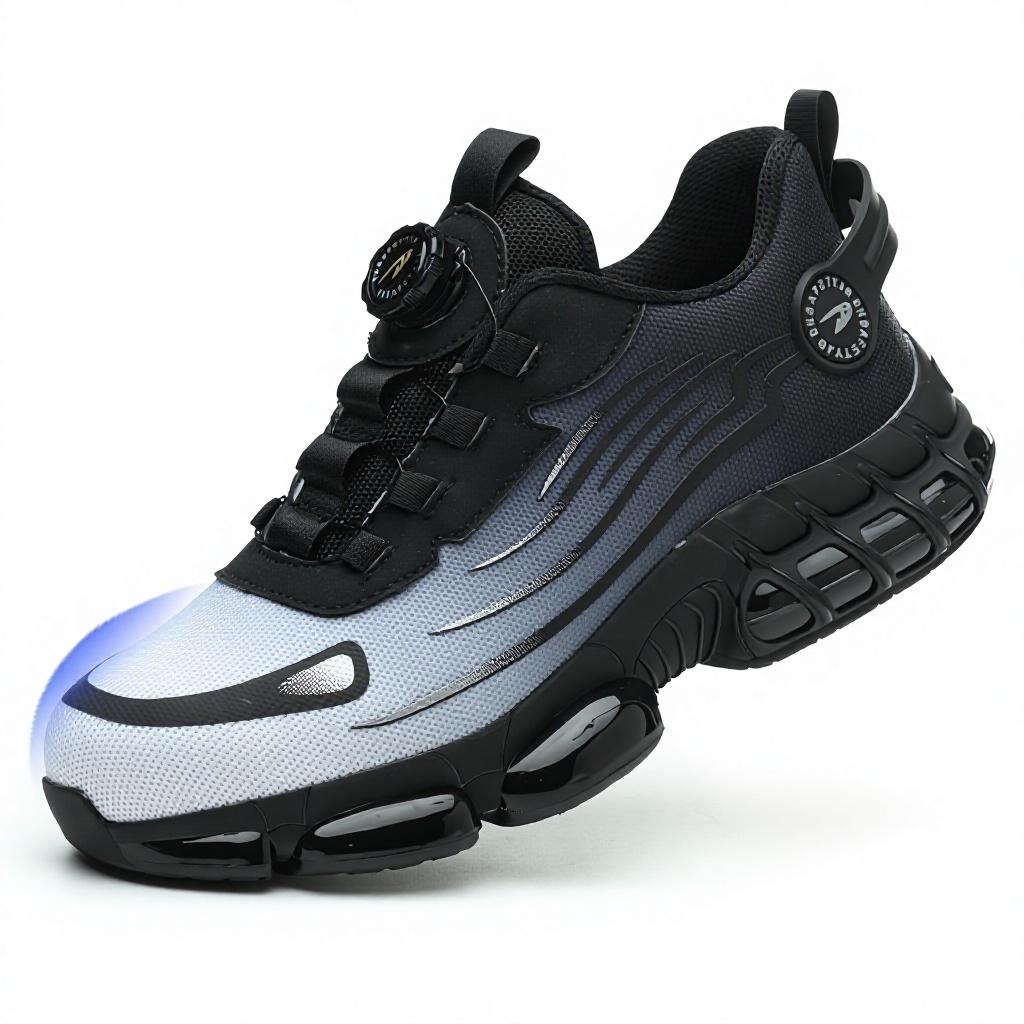
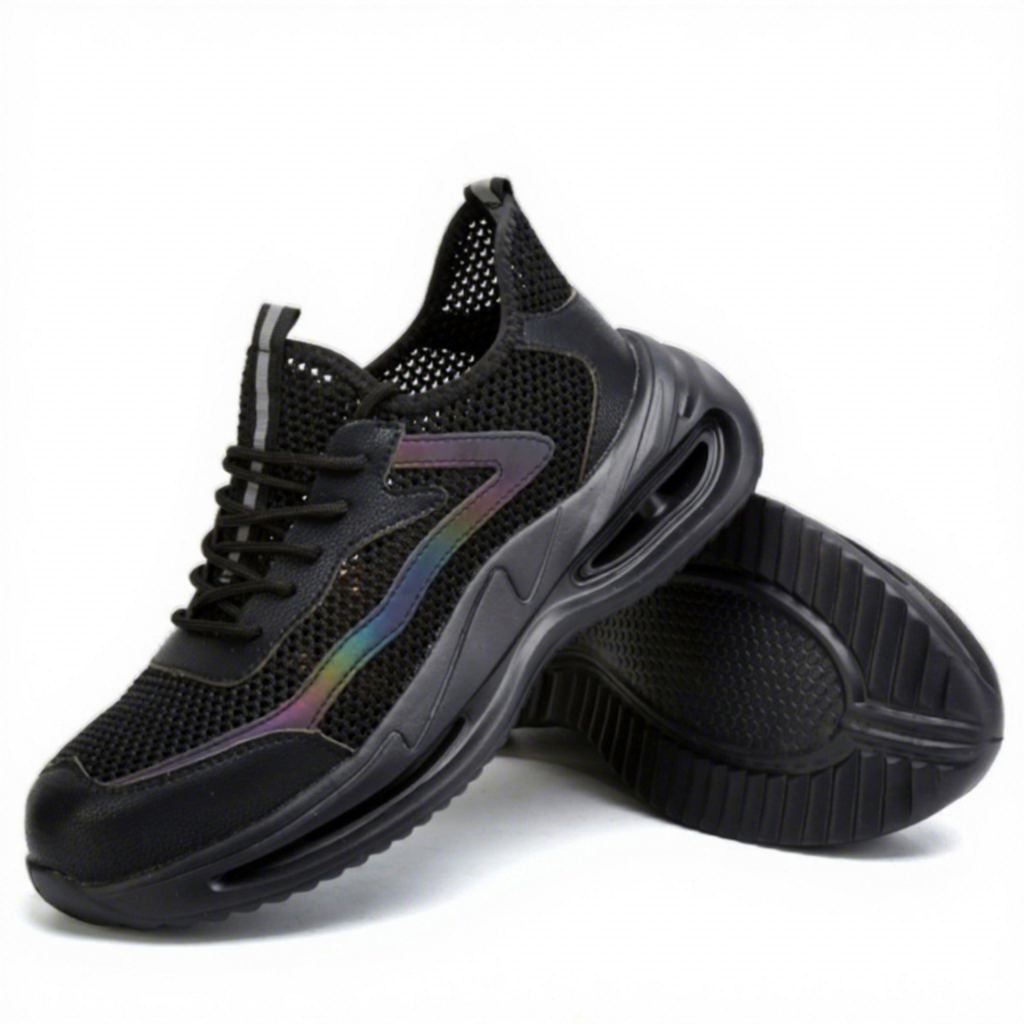
Quality Audit Zones
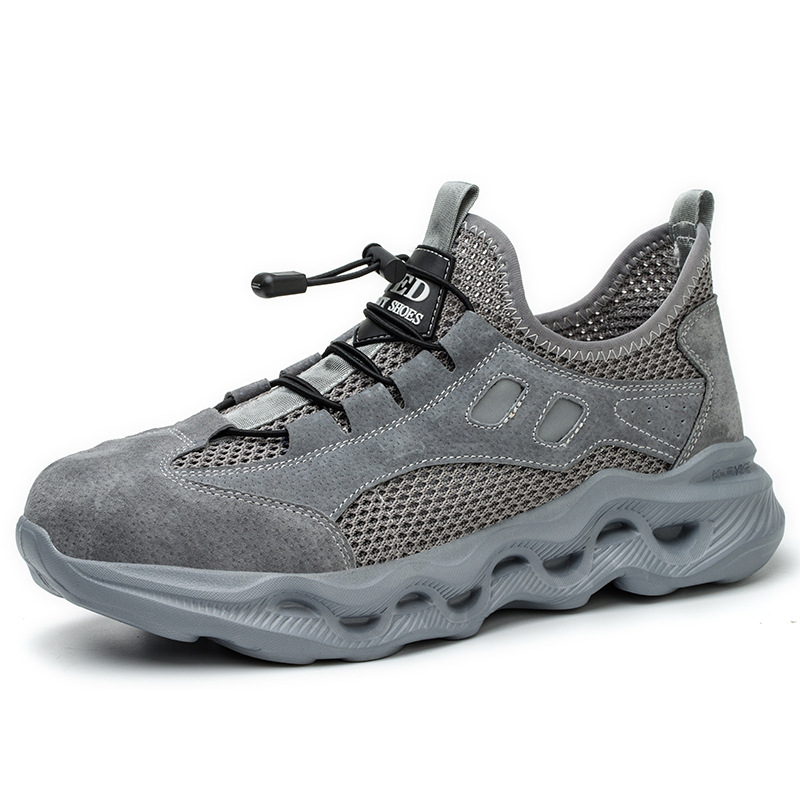
Men's Summer Low Top Breathable Odor-Resistant Steel Cap Ultra-Light
Product Specs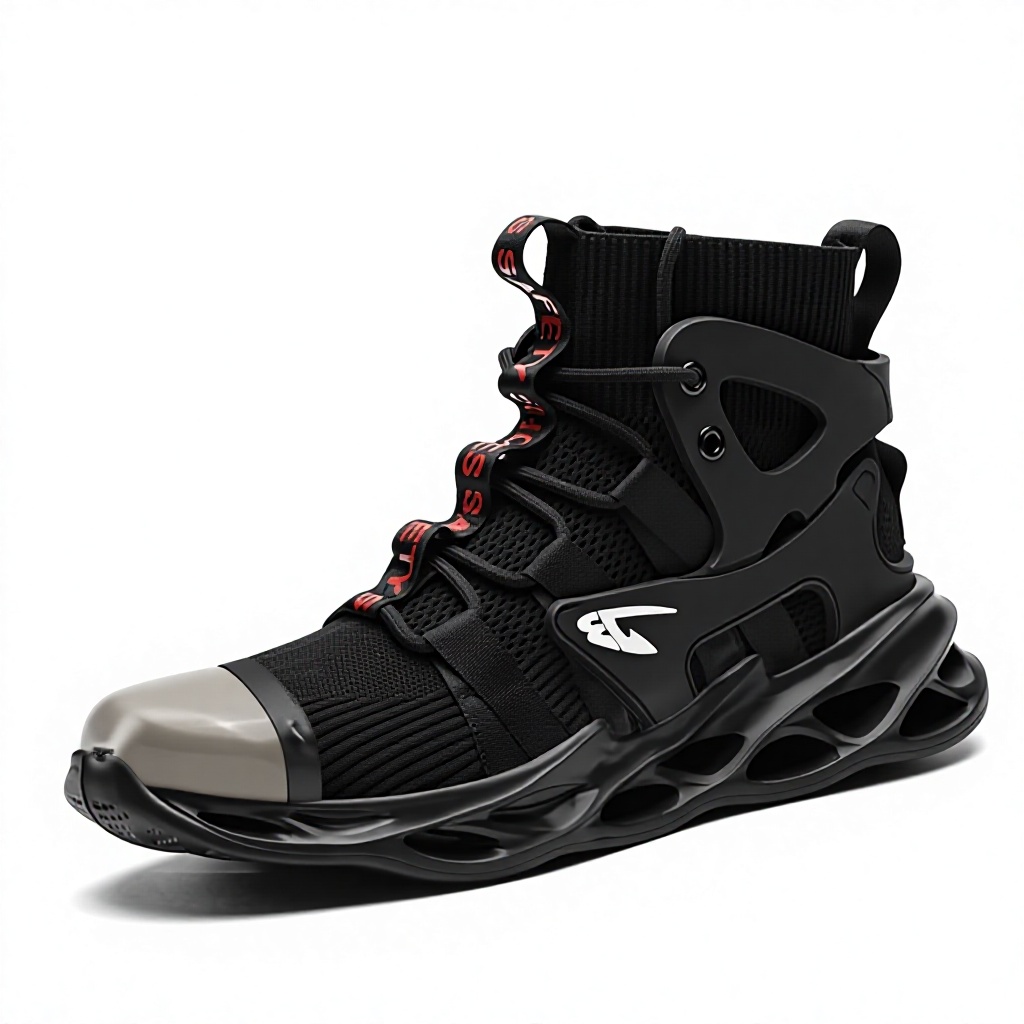
200J
Kinetic Impact Rating (EN ISO 20345)
15kN
Compression Resistance Margin
300°C
HRO Contact Heat Endurance (60s)
100%
Dielectric Non-Metallic Inspection
Technical Specification Guide: Why Tyre Manufacturing Demands Specialized Composite Toe Footwear
Tyre manufacturing represents one of the most mechanically and chemically taxing industrial environments in modern manufacturing. From initial polymer compounding and Banbury internal mixers to carbon black handling, steel belt calendering, tire building, green tire handling, and final vulcanization presses, worker footwear faces simultaneous threats. Standard commercial safety shoes fail rapidly due to aromatic processing oils, heavy plasticizer leaching, high radiant vulcanizing mold temperatures (frequently exceeding 160°C to 200°C), and micro-puncture hazards generated by loose brass-coated steel cord offcuts.
Procurement engineers and occupational health directors operating under European PPE Regulation (EU) 2016/425 prioritize CE-certified composite toe footwear over legacy metallic footwear for several critical reasons:
Thermal Bridging Prevention
Unlike steel toe caps that conduct radiant heat directly to the toe box near steam-heated curing presses, engineering polymers (carbon fiber and fiberglass) act as thermal insulators, preventing blister formation and skin necrosis during 12-hour factory shifts.
Cord Splinter Puncture Protection
Tire bead winding and steel breaker cutting lines produce microscopic needle-sharp wire fragments. Non-metallic anti-puncture aramid/Kevlar midsoles provide 100% plant surface coverage, preventing punctures where steel midsoles leave peripheral gaps.
ESD & Flammable Atmosphere Safe
Volatile hydrocarbon tackifying resins and solvent vapor zones in inner-liner coating bays require strictly controlled ESD dissipation (100 kΩ to 35 MΩ) to prevent static discharges that can trigger fire emergencies in solvent storage areas.
Controlled Production
Verified Supply Chain & Manufacturing Excellence
Originating from our precision manufacturing center in Zhejiang, we build durability into every layer through locked bill-of-materials and documented QA testing.
Locked Bill-of-Materials (BOM)
Repeat supply consistency is guaranteed. We qualify established high-tenacity composite caps, slip-resistant dual-density PU/Nitrile rubber outsoles, and locked supplier specifications so replacement pairs perform identically to trial test units.
Onsite TÜV & CE Documentation
Our production protocols are vetted under ISO 9001 quality systems. We furnish authentic CE Certificates (EN ISO 20345:2022 S1P, S2, S3, HRO, ESD, SRC), complete test reports, and customs clearing documentation directly with every commercial container.
Custom OEM / ODM Program
Custom tread molds, corporate color accents, laser-branded uppers, custom fit-dial lace mechanisms, and customized packaging are fully supported for OEM shoe brands, industrial safety distributors, and tire manufacturing conglomerates.
Factory Deployment
Localized Tyre Production Workplace Application Scenarios
Targeted footwear performance matched to specific mechanical, chemical, and thermal zones across the tire fabrication lifecycle.


Engineering Matrix
Safety Footwear Selection Matrix for Tyre Plants
Cross-reference your workshop zone hazards against verified CE standard designations.
| Tyre Plant Department | Primary Hazard Exposure | Recommended Protection | Upper & Outsole Engineering | CE Standard Requirement |
|---|---|---|---|---|
| Compounding & Mixing | Aromatic oils, polymer resin spills, heavy carbon dust | Composite Toe + FO Resistance | Seamless Microfiber upper + Nitrile oil-proof sole | EN ISO 20345:2022 S2 / S3 FO SR |
| Steel Belt Slitting | Sharp steel cord ends, cut offcuts on floor | Aramid Non-Metal Midsole (PL) | High-density Kevlar midsole (1100N puncture resistance) | EN ISO 20345:2022 S1P / S3 PL |
| Curing & Vulcanization | 160°C–200°C radiant heat, steam condensation, hot mold contact | HRO Heat Resistance + Insulative Cap | Thermal composite cap + 300°C vulcanized rubber sole | EN ISO 20345:2022 S1 HRO HI CI |
| Tire Assembly & Logistics | Heavy green tires, transport cart collisions, long walking shifts | Lightweight Ergonomic Fly-knit | Breathable mesh upper + Ultra-rebound EVA/Rubber sole | EN ISO 20345:2022 S1 ESD SR |
Localized Trends in Global Tyre Manufacturing Personal Protective Equipment (PPE)
Across key tire manufacturing epicenters—including Central and Eastern Europe (Poland, Czech Republic, Romania), Southeast Asia (Thailand, Vietnam, Indonesia), and the Americas (Mexico, USA)—industrial safety footwear procurement is shifting rapidly away from low-cost, disposable boots toward high-durability ergonomic foot systems.
Three distinct industry trends govern modern factory tenders:
1. Decarbonization and Lightweight Ergonomics: Operators walk an average of 14,000 to 18,000 steps daily on hard concrete. Heavy steel boots contribute significantly to knee joint strain, lower spine fatigue, and increased lost-time injury (LTI) rates. Transitioning to lightweight composite toe caps (up to 45% lighter than steel) with athletic EVA compound cushion soles reduces plant fatigue markers by up to 28%.
2. Transition to Metal-Free Facility Access: Modern tire production centers incorporate automated automated guided vehicles (AGVs), laser scanners, and security metal detection gates between warehouse and production modules. 100% metal-free composite footwear (composite toe cap + aramid textile penetration midsole + non-metallic eyelets) allows workers to pass through inspection zones without triggering security protocols.
3. Increased Chemical Resistance to Silicone and Processing Plasticizers: Uncured rubber compounds contain compounding plasticizers and mould release sprays (silicone emulsions) that degrade standard PU soles through polymer chain dissolution. Next-generation tire plant footwear incorporates dual-density PU/Rubber blends formulated to resist hydrocarbon decomposition.
Buyer Knowledge Base
Frequently Asked Questions by Industrial Sourcing Teams
Direct answers regarding testing certifications, OEM customization, import documentation, and minimum order terms.
Why choose composite toe caps over steel caps for tire plants?
Composite caps (fiberglass, carbon fiber, or reinforced poly-resin) do not conduct thermal energy, maintaining an insulated toe box near hot vulcanization mold presses. They also rebound back without pinching toes upon sudden impact, are 40-50% lighter than carbon steel, and are 100% non-magnetic and metal-detector friendly.
What CE safety shoe certificates do you provide with consignments?
We supply full CE test documentation under EN ISO 20345:2022 from notified European testing bodies (such as CTC, SATRA, or TÜV Rheinland). Reports verify 200J toe impact resistance, 15kN compression, antistatic/ESD performance, slip resistance (SR), and contact heat resistance (HRO).
What trade terms and currency settlements are supported?
We support comprehensive global trade terms: FOB, CFR, CIF, EXW, FAS, FCA, CPT, DDP, and DDU. Payment options include flexible T/T, L/C at sight, and commercial credit, with multi-currency settlements in USD, EUR, CAD, AUD, GBP, and CNY.
What is your OEM/ODM private label minimum order quantity (MOQ)?
Standard OEM production with customized branding, tailored shoe boxes, and upper logo stamping starts from 500 to 1,000 pairs per style. Trial batch sampling and plant audit trial orders can be coordinated with our engineering account directors.
Protect Your Tyre Plant Workforce with Engineered Safety Footwear
Request comprehensive EN ISO 20345:2022 laboratory test reports, commercial price matrixes, and physical trial samples directly from our factory engineering team.
Send an Inquiry